Our Products
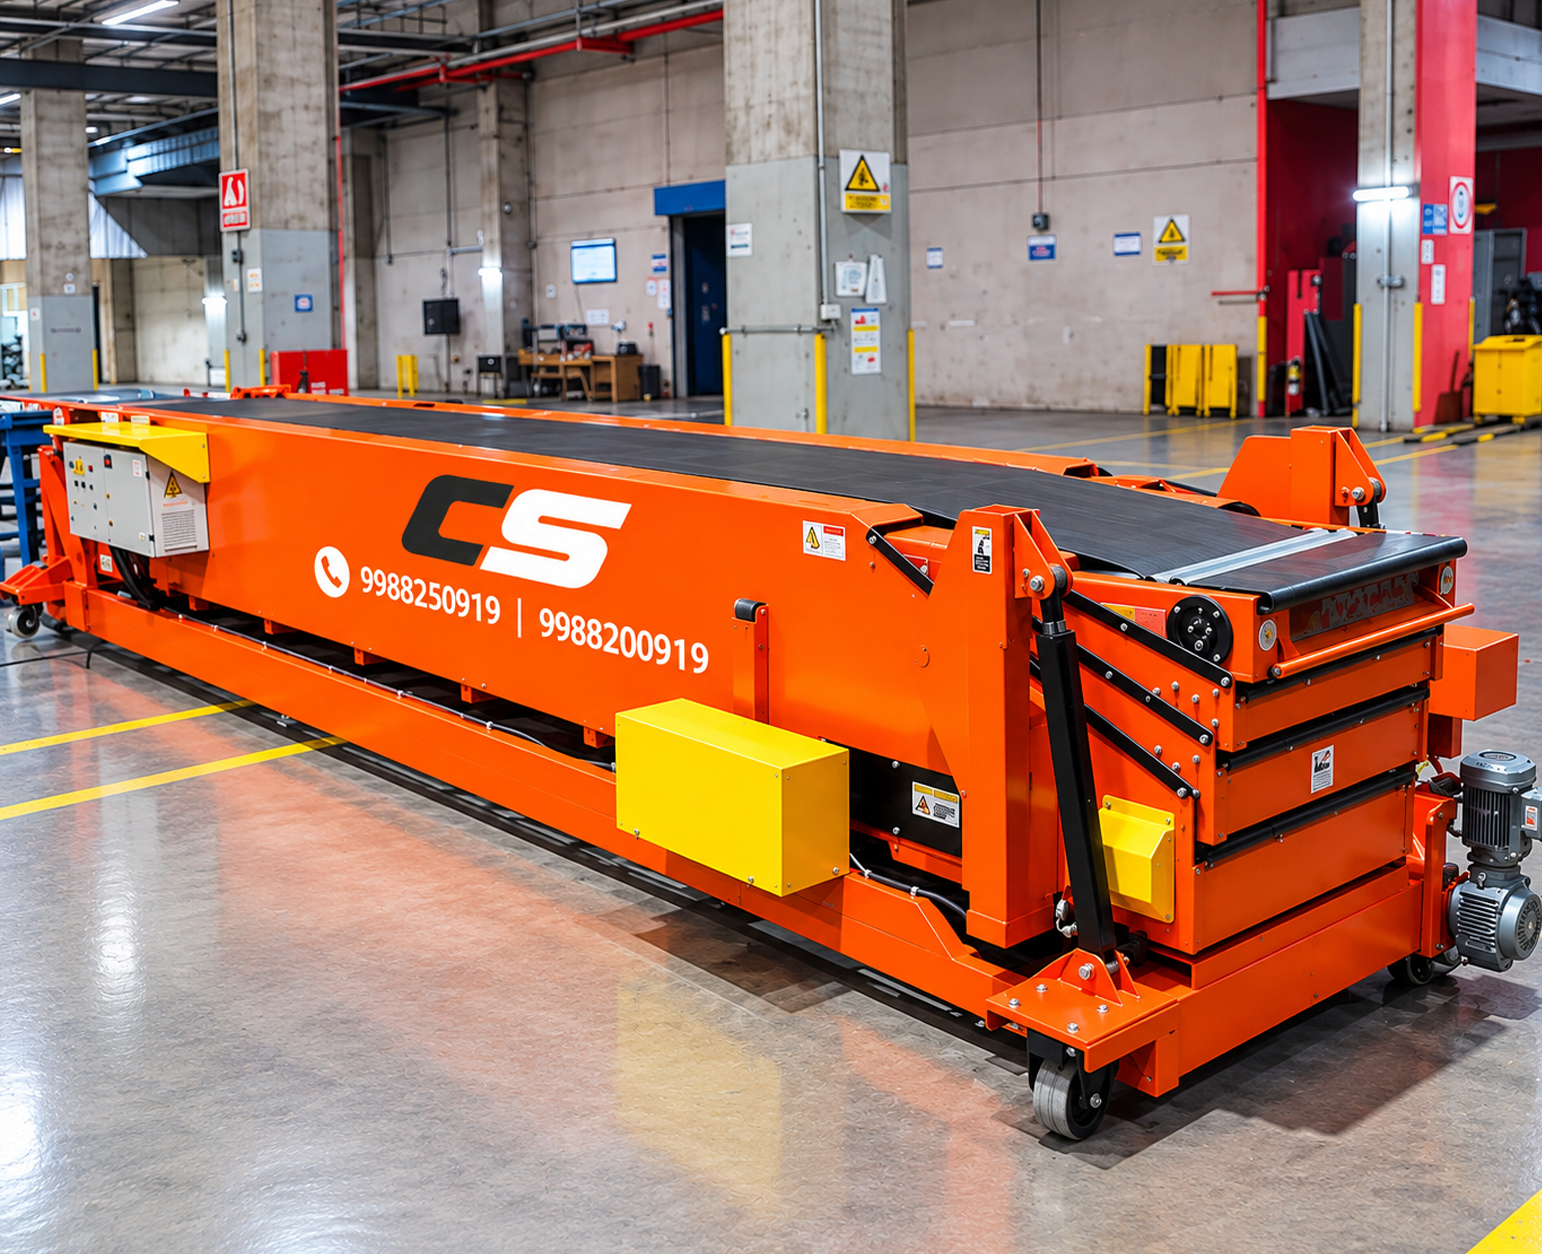
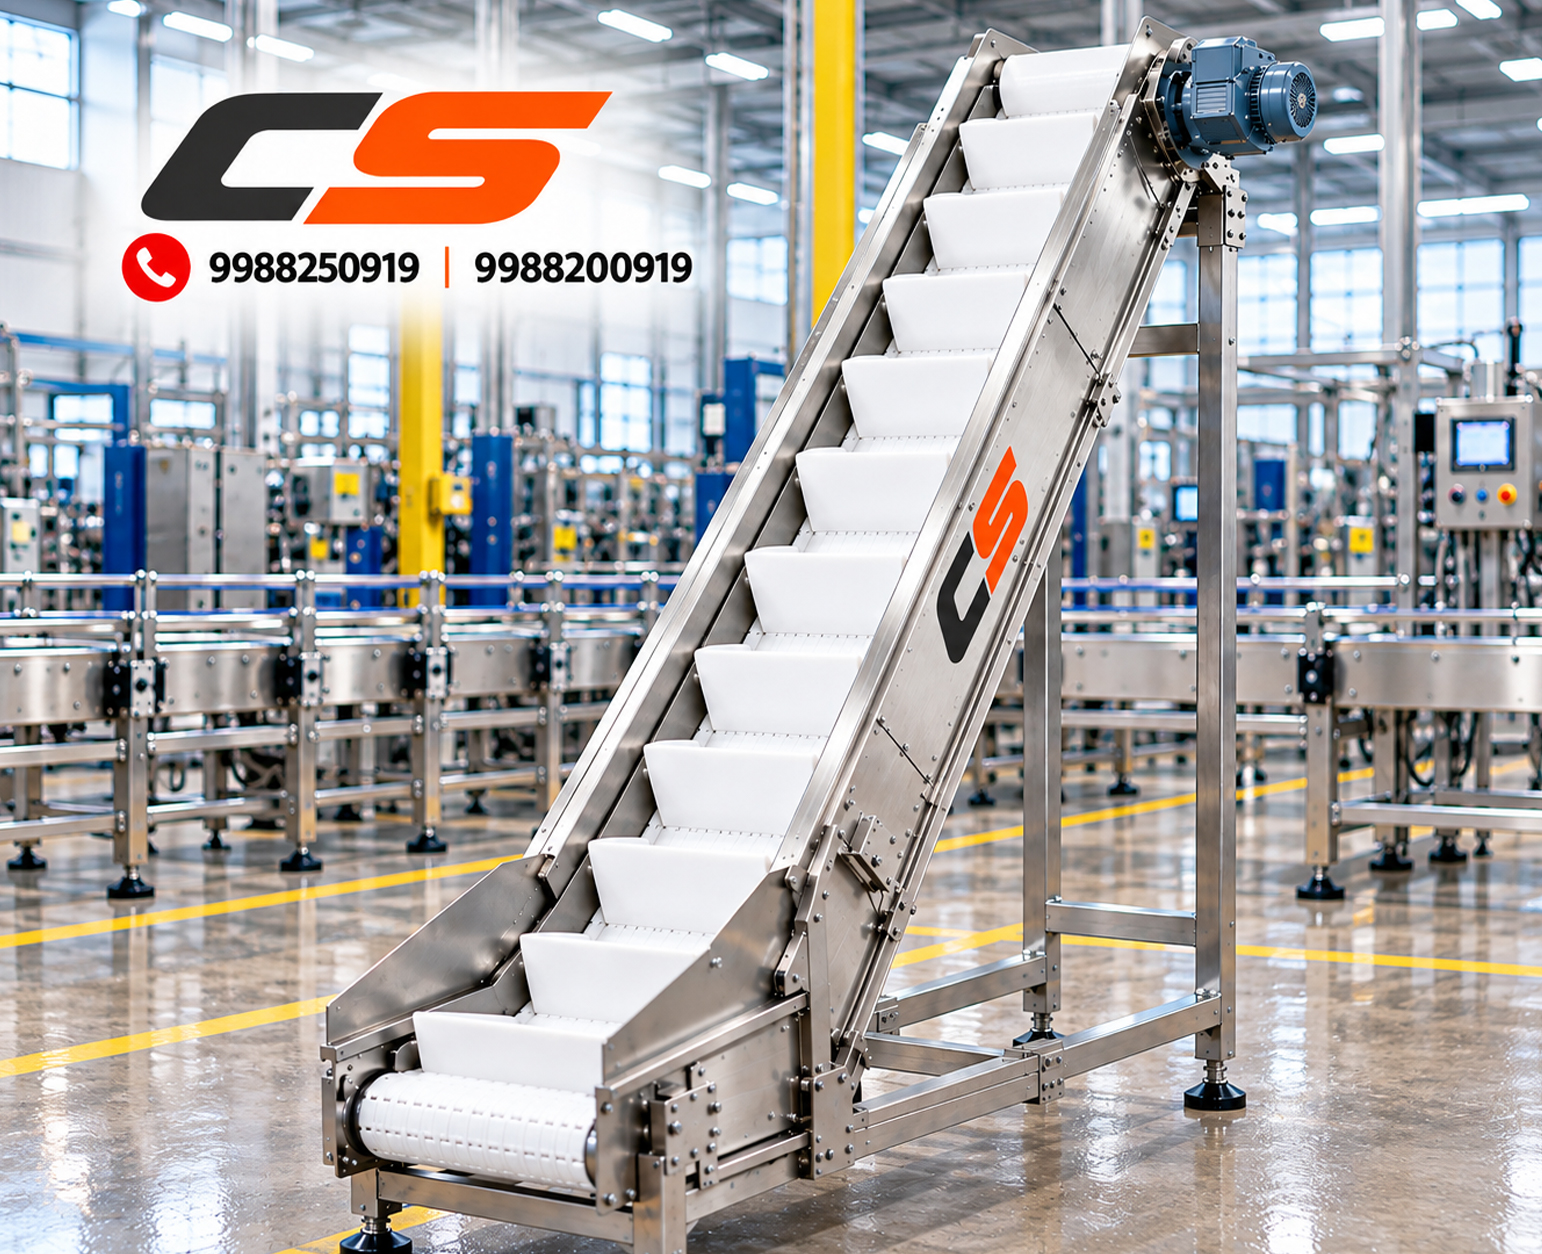
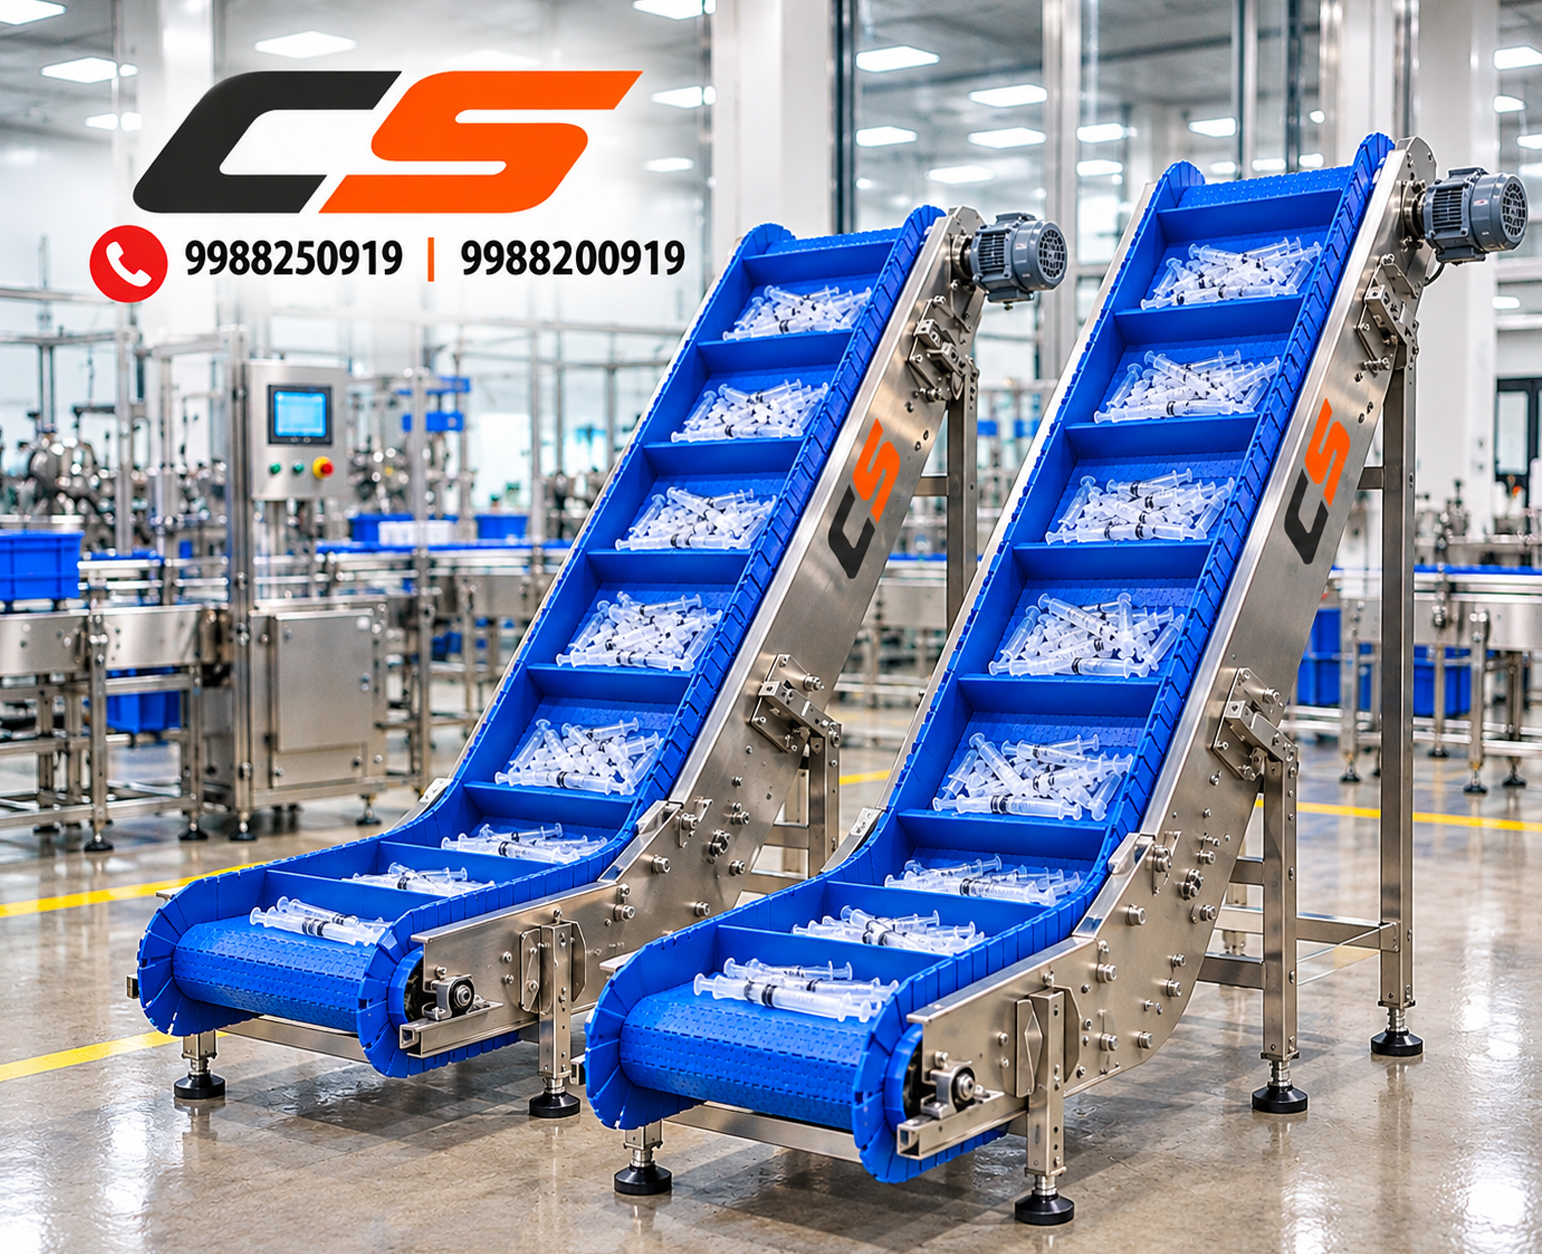
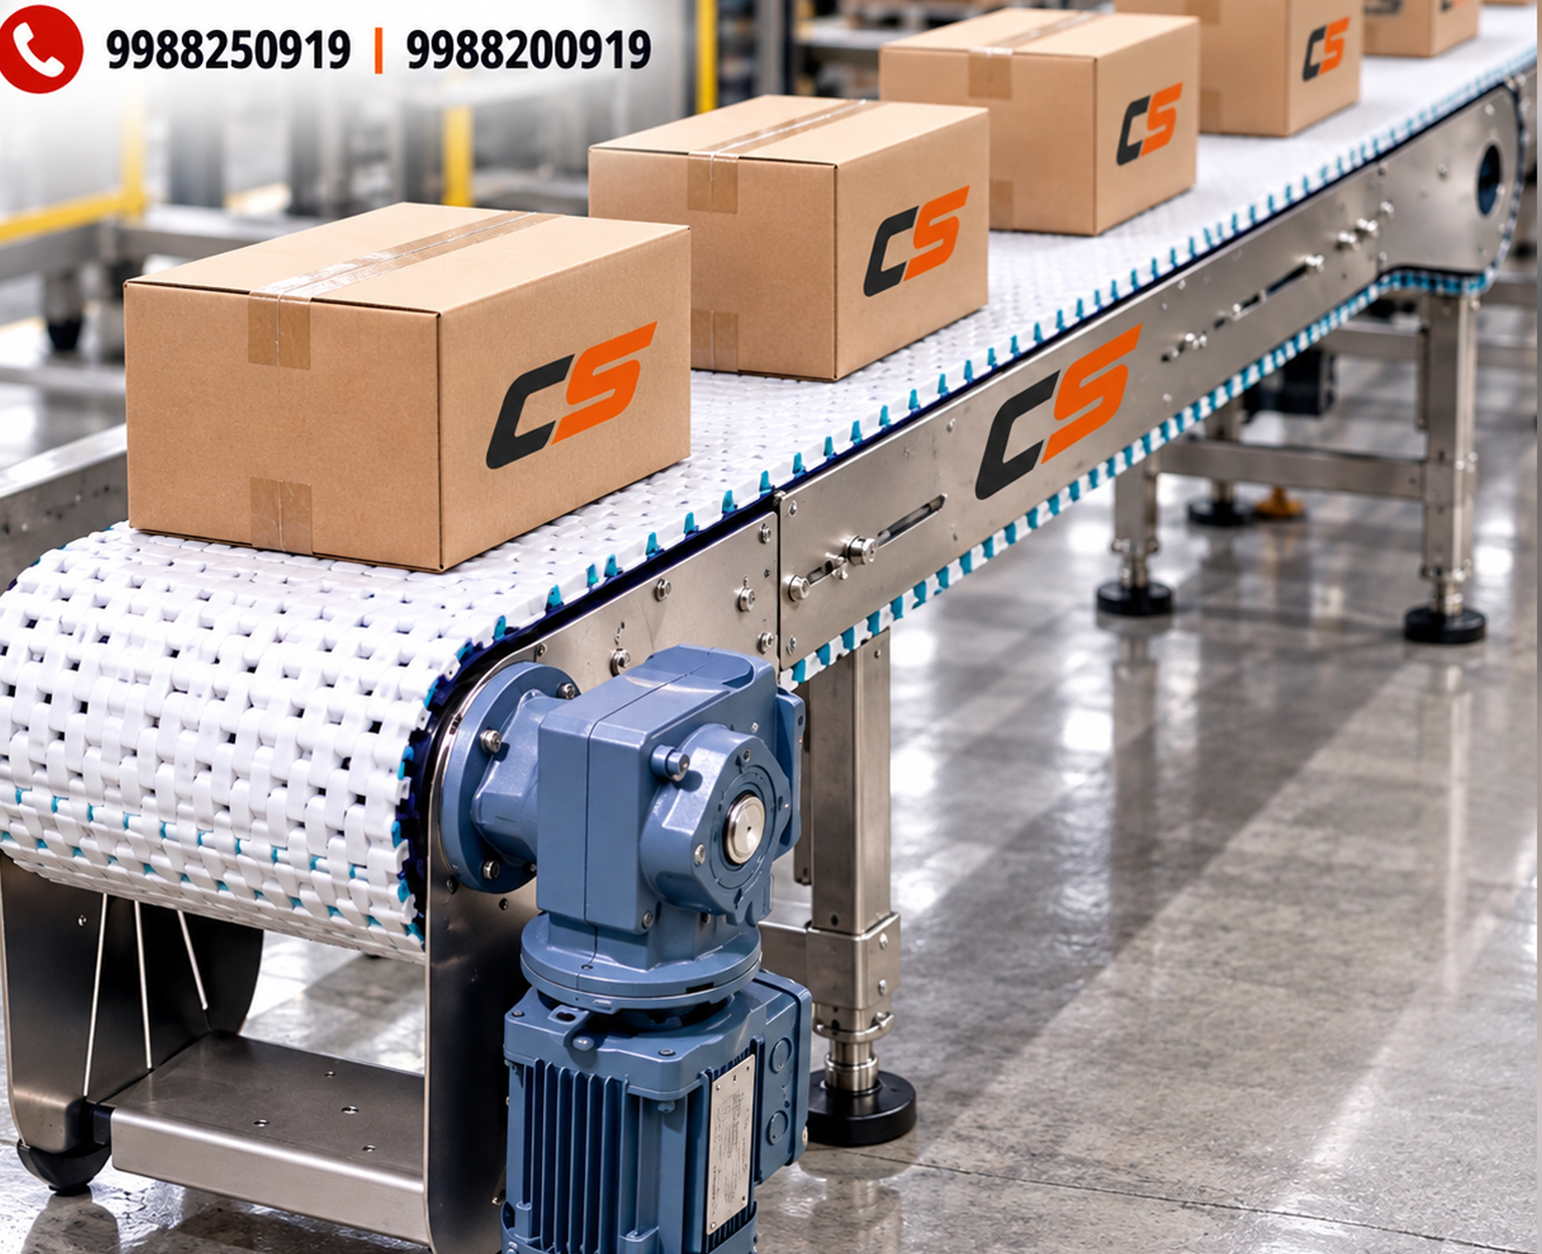
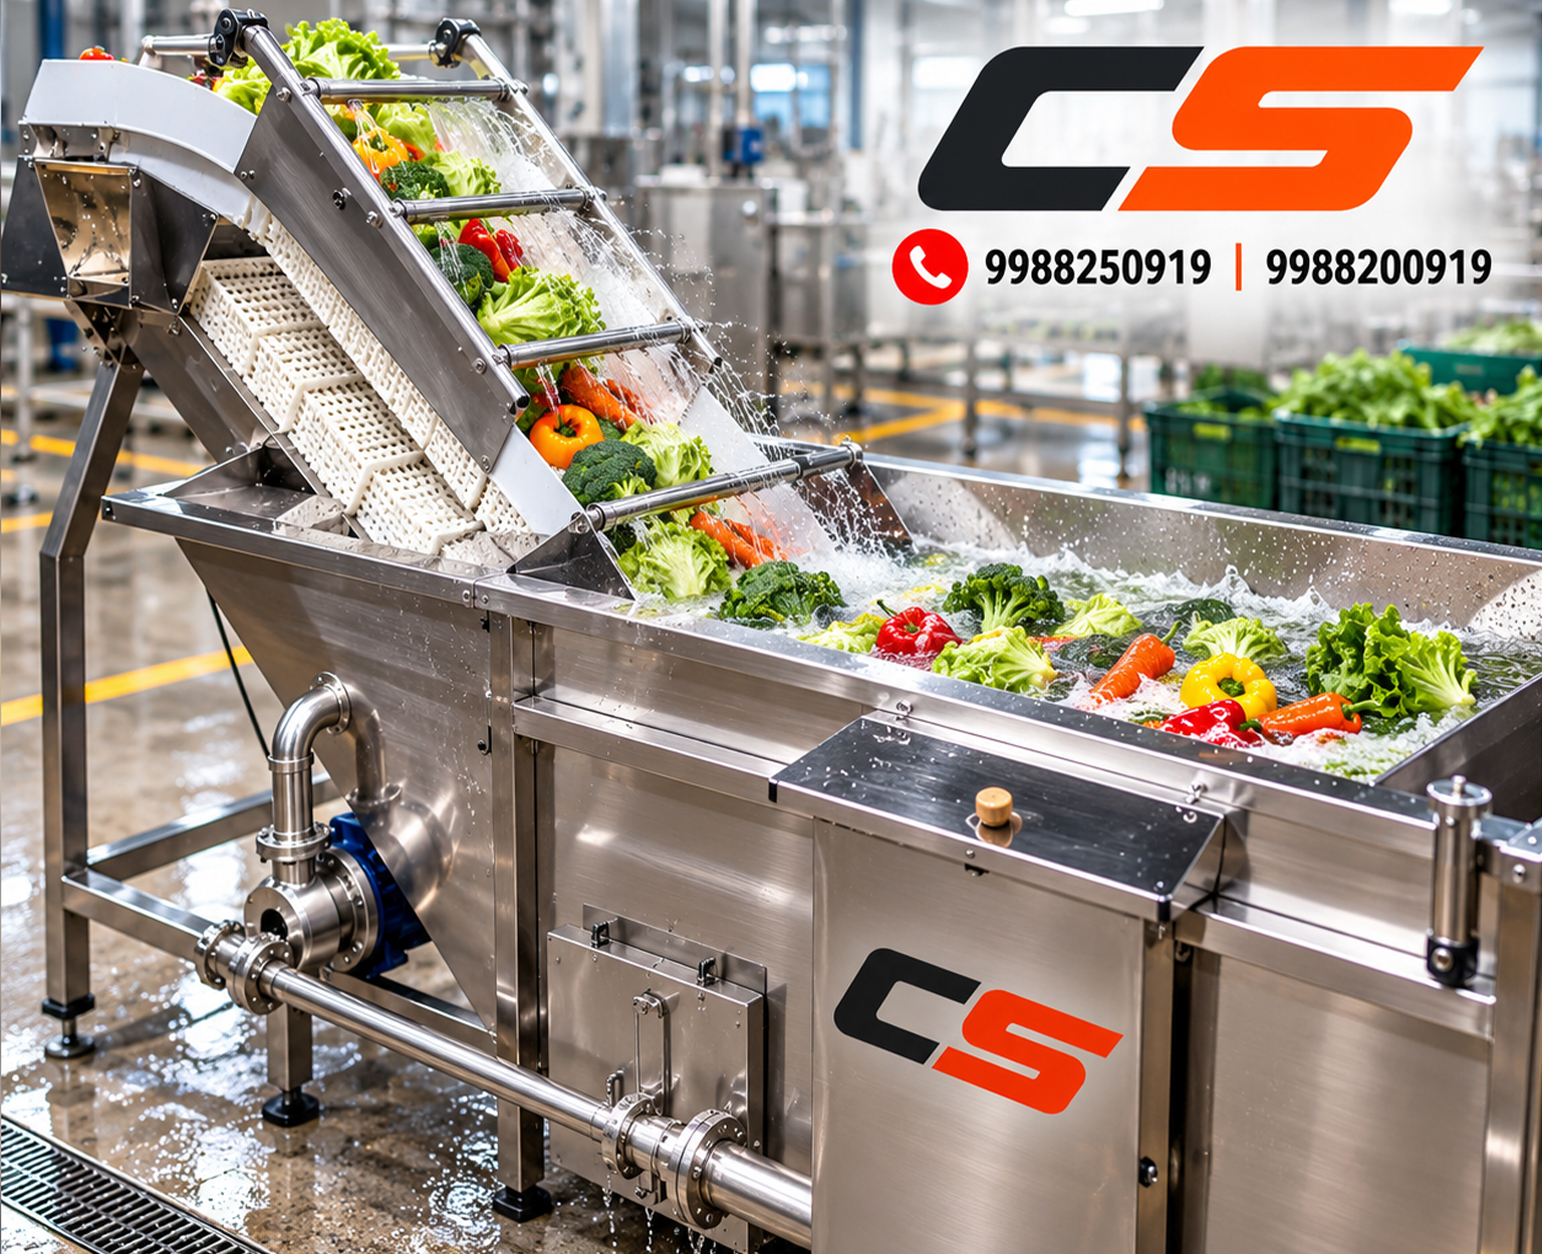
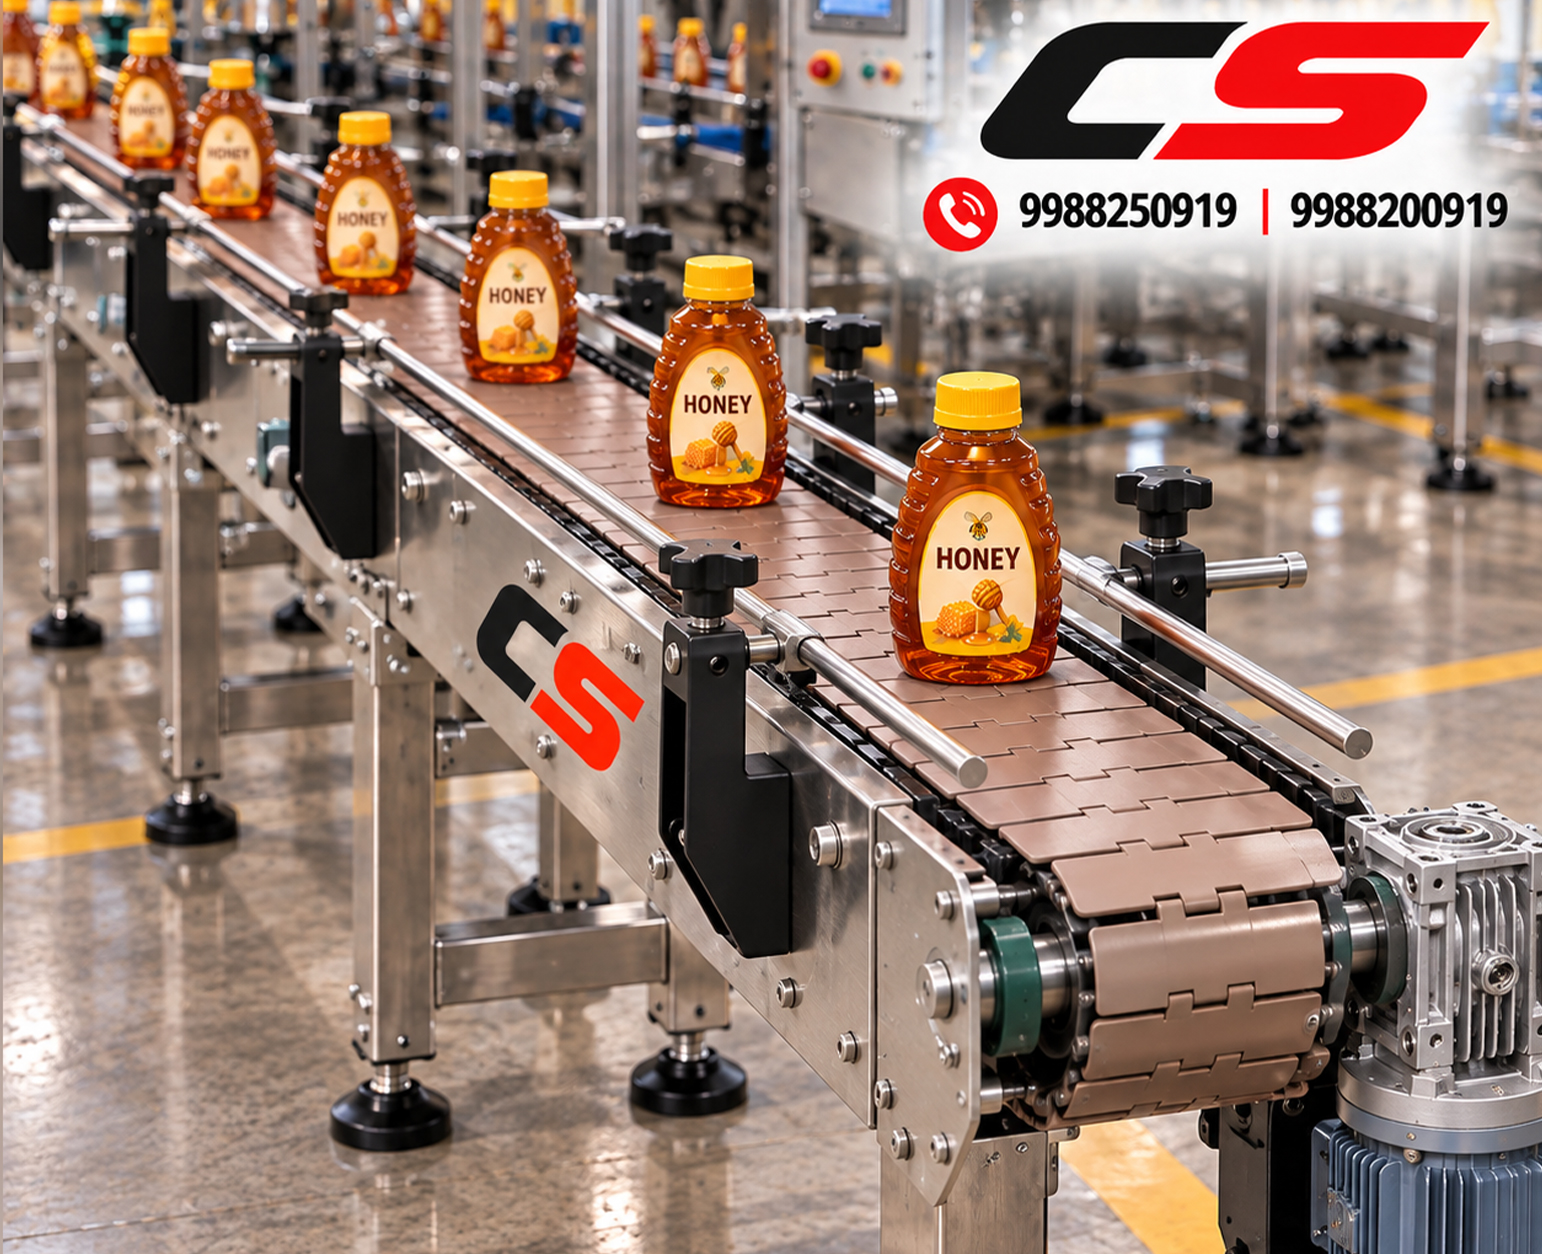
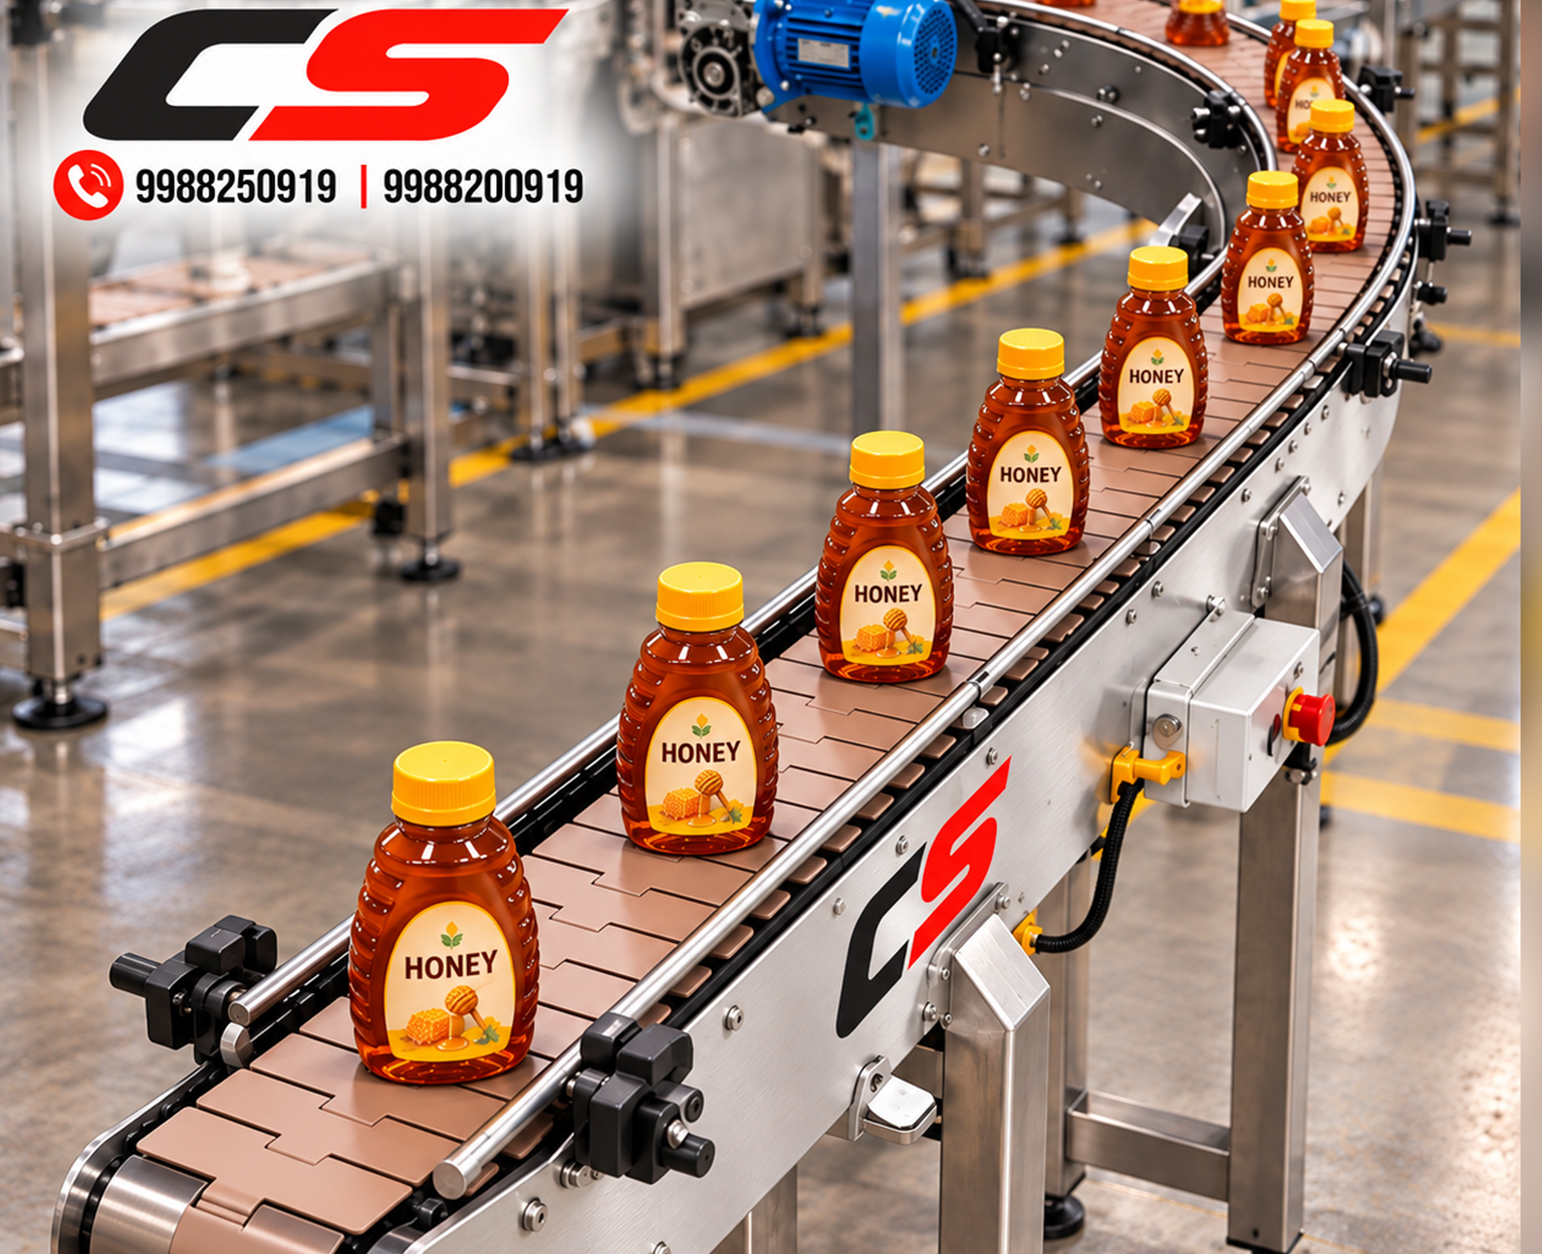
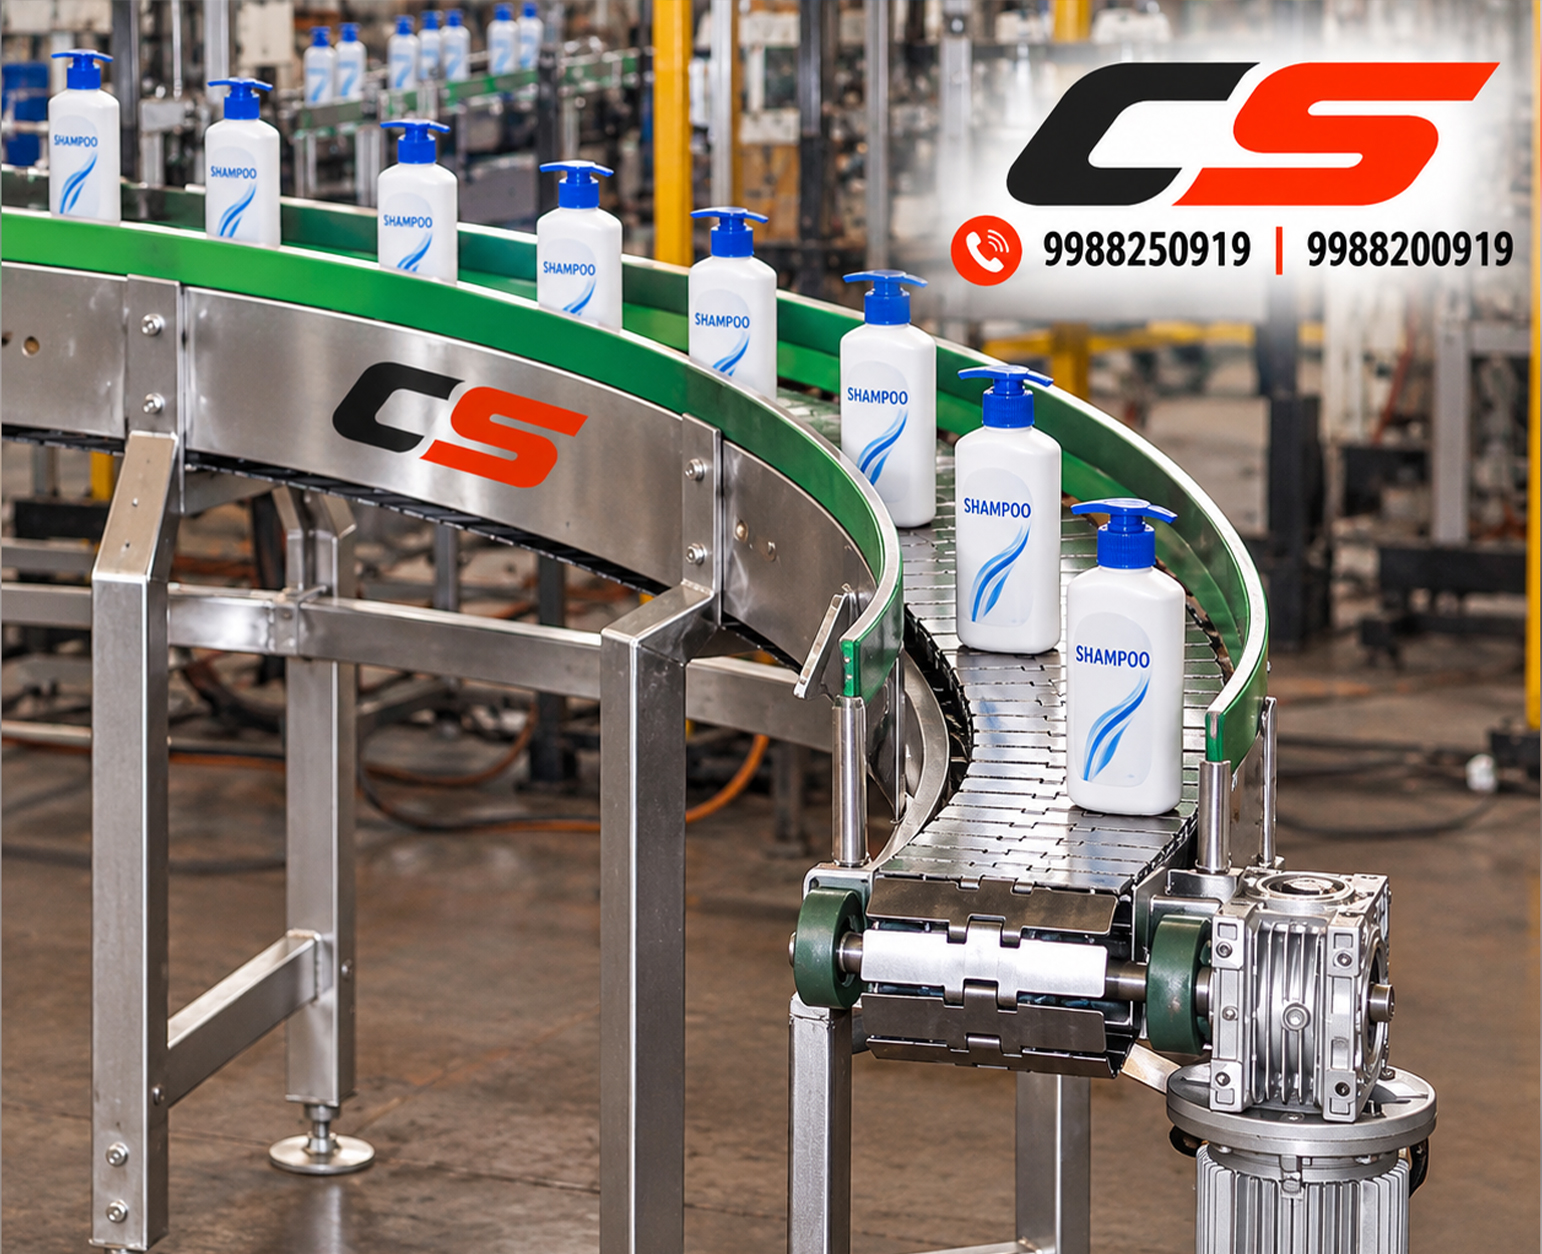
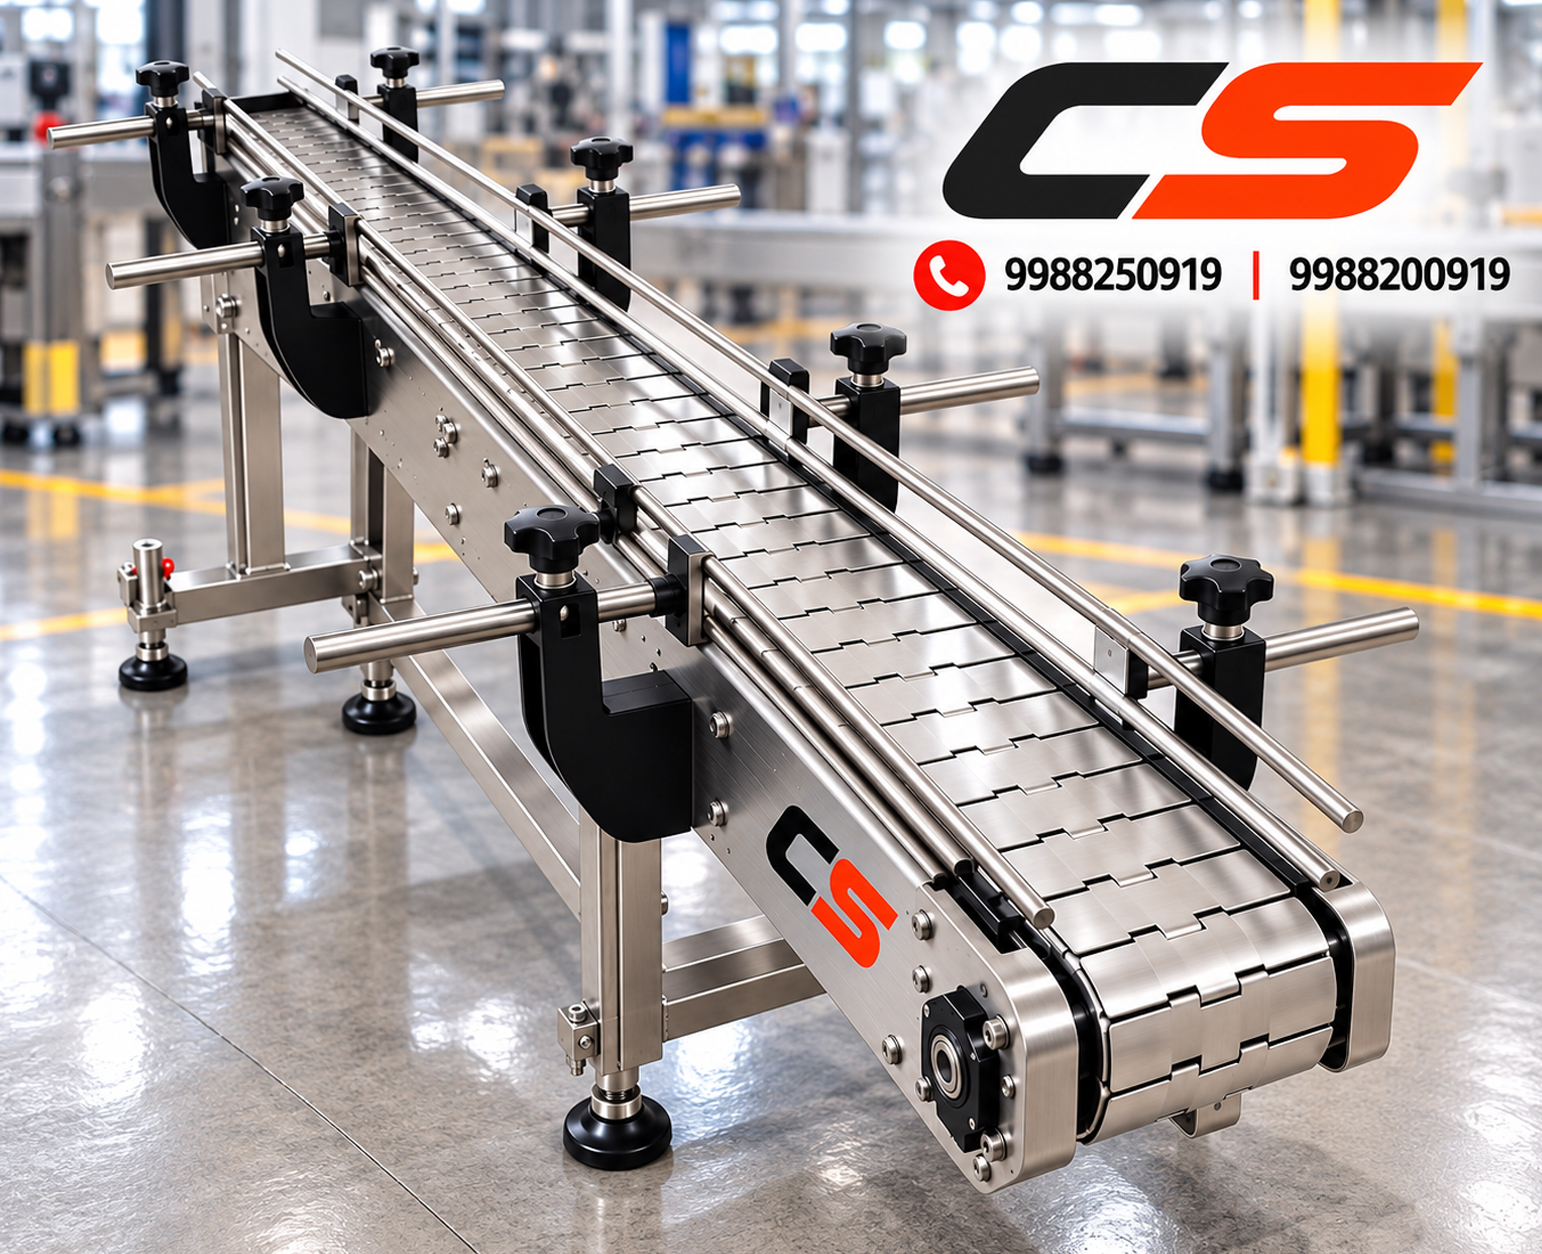
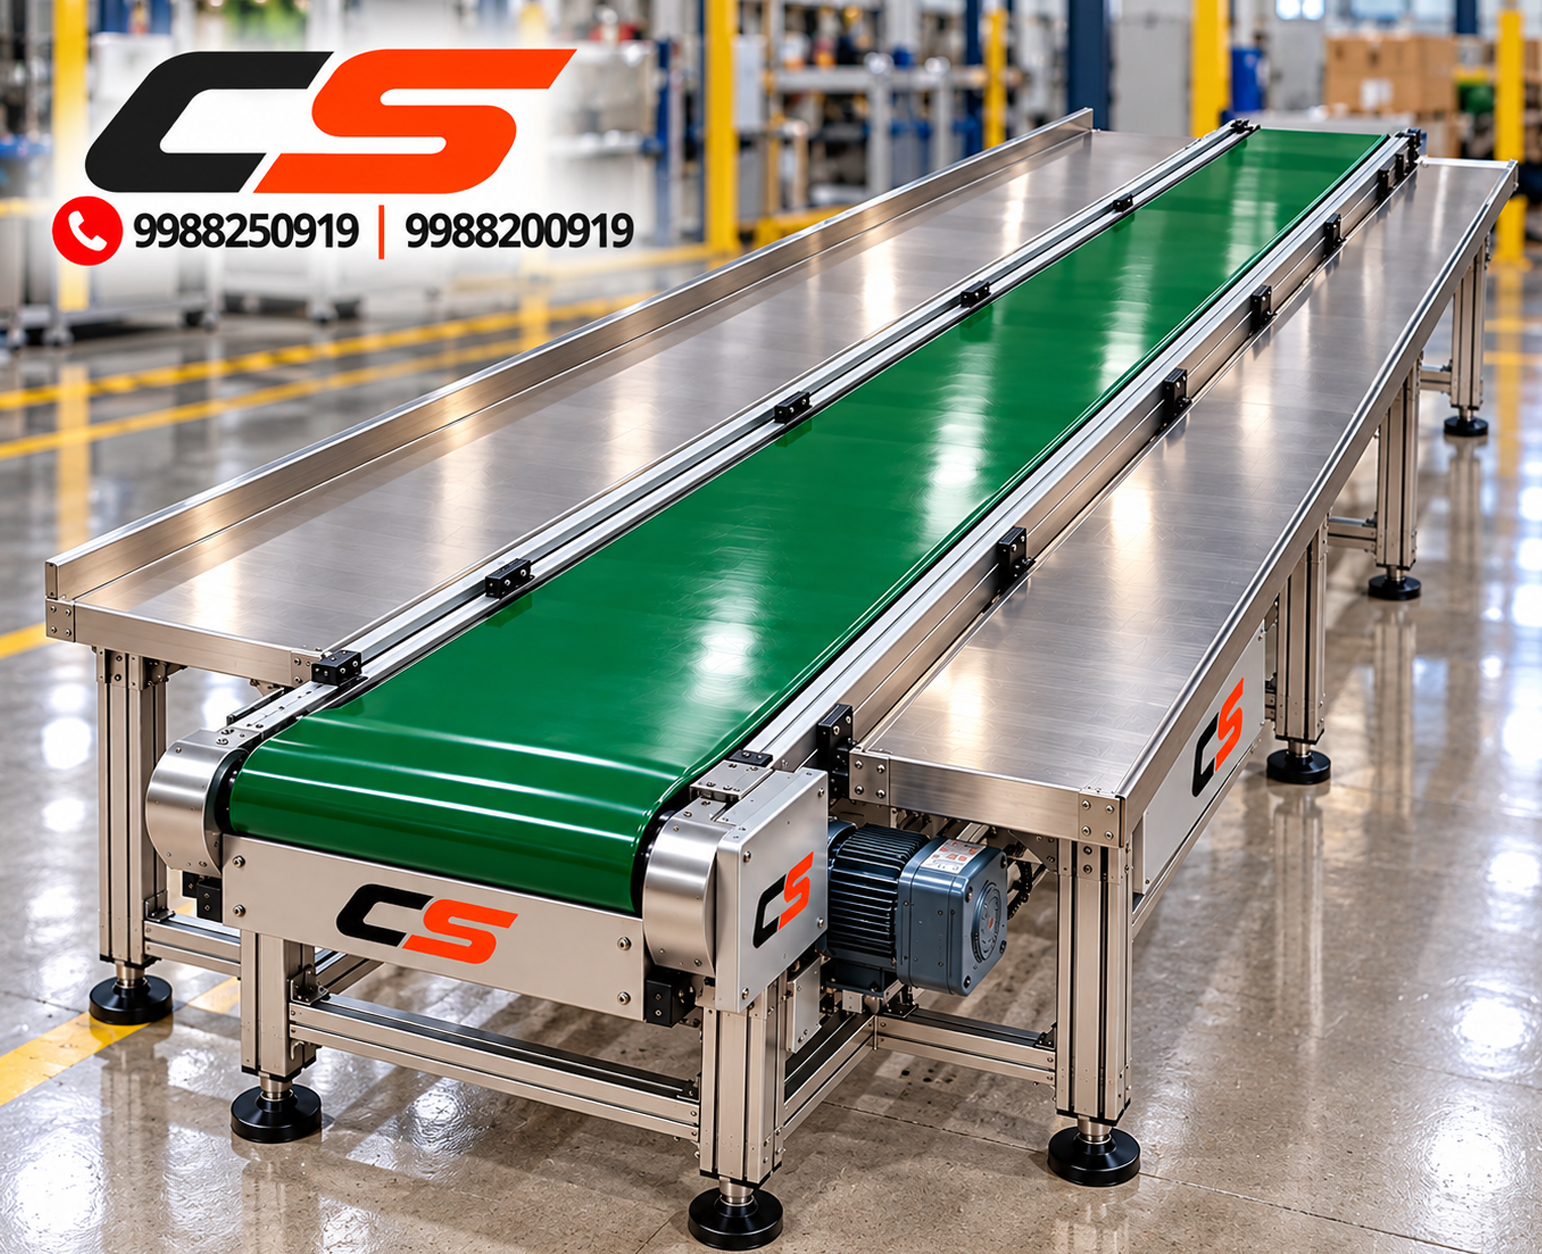
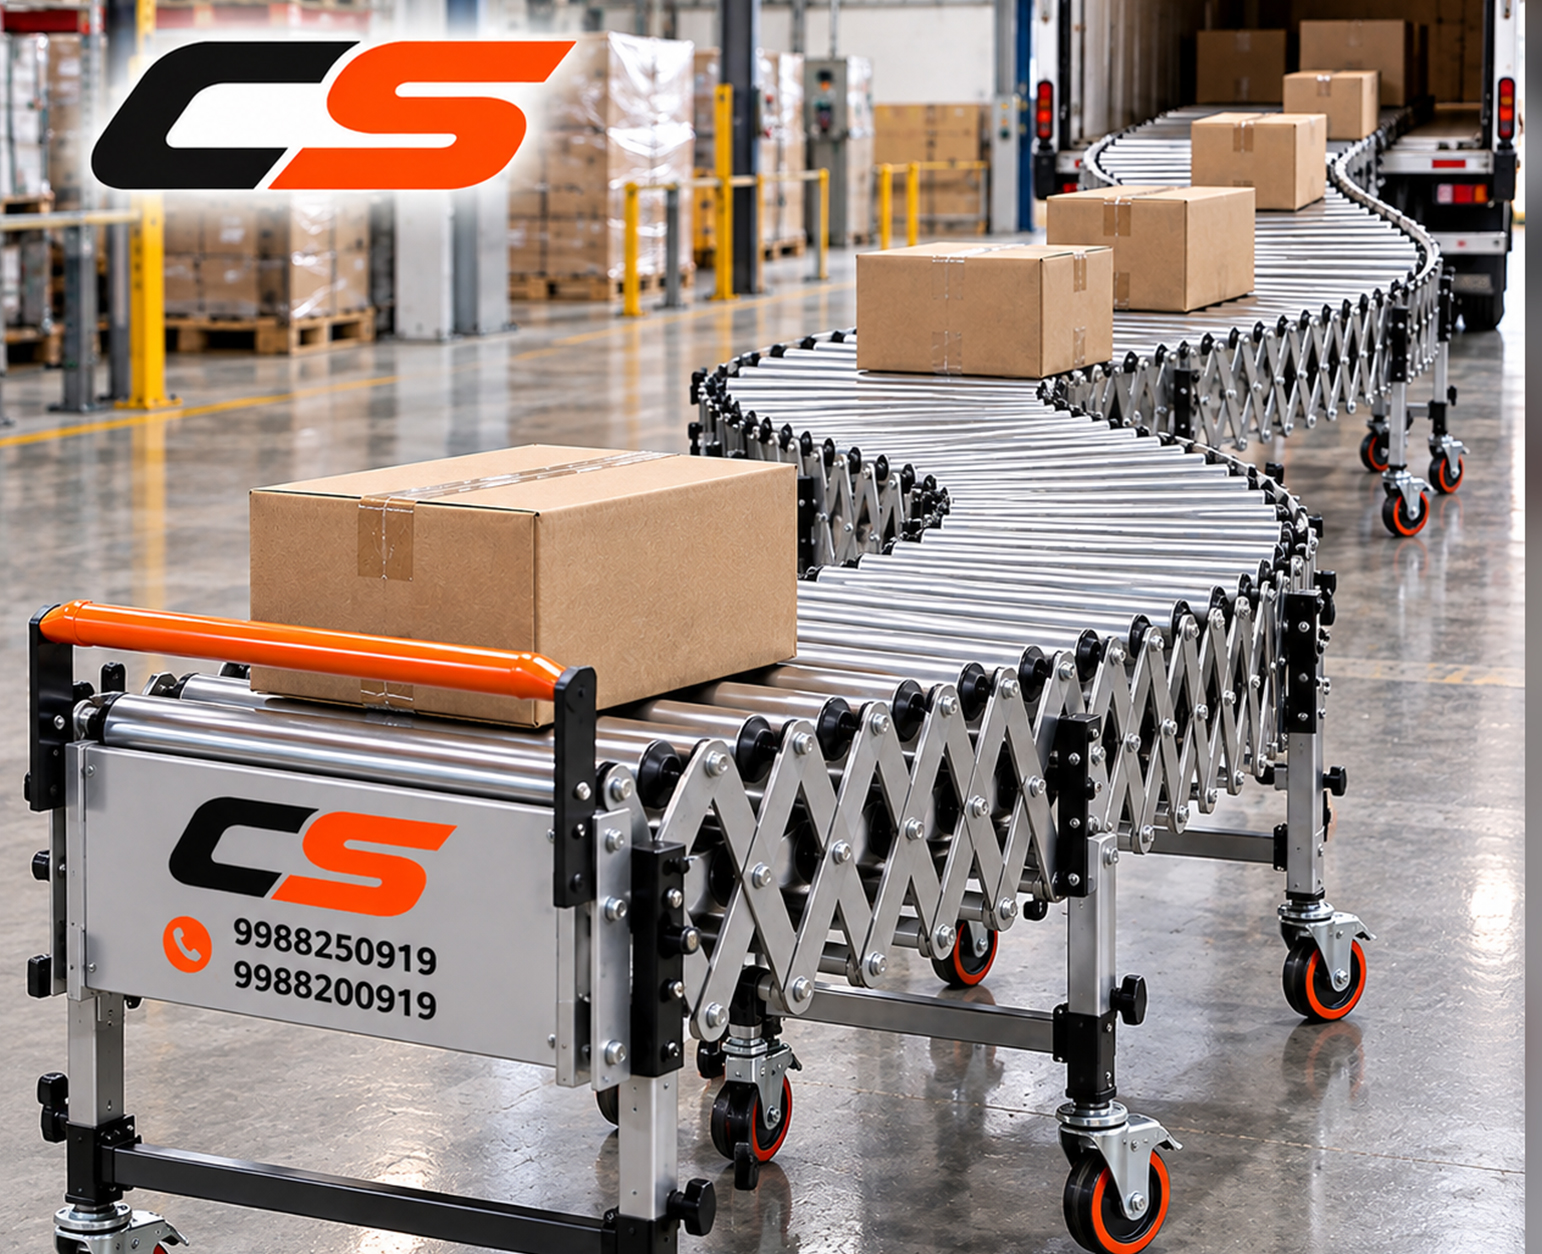
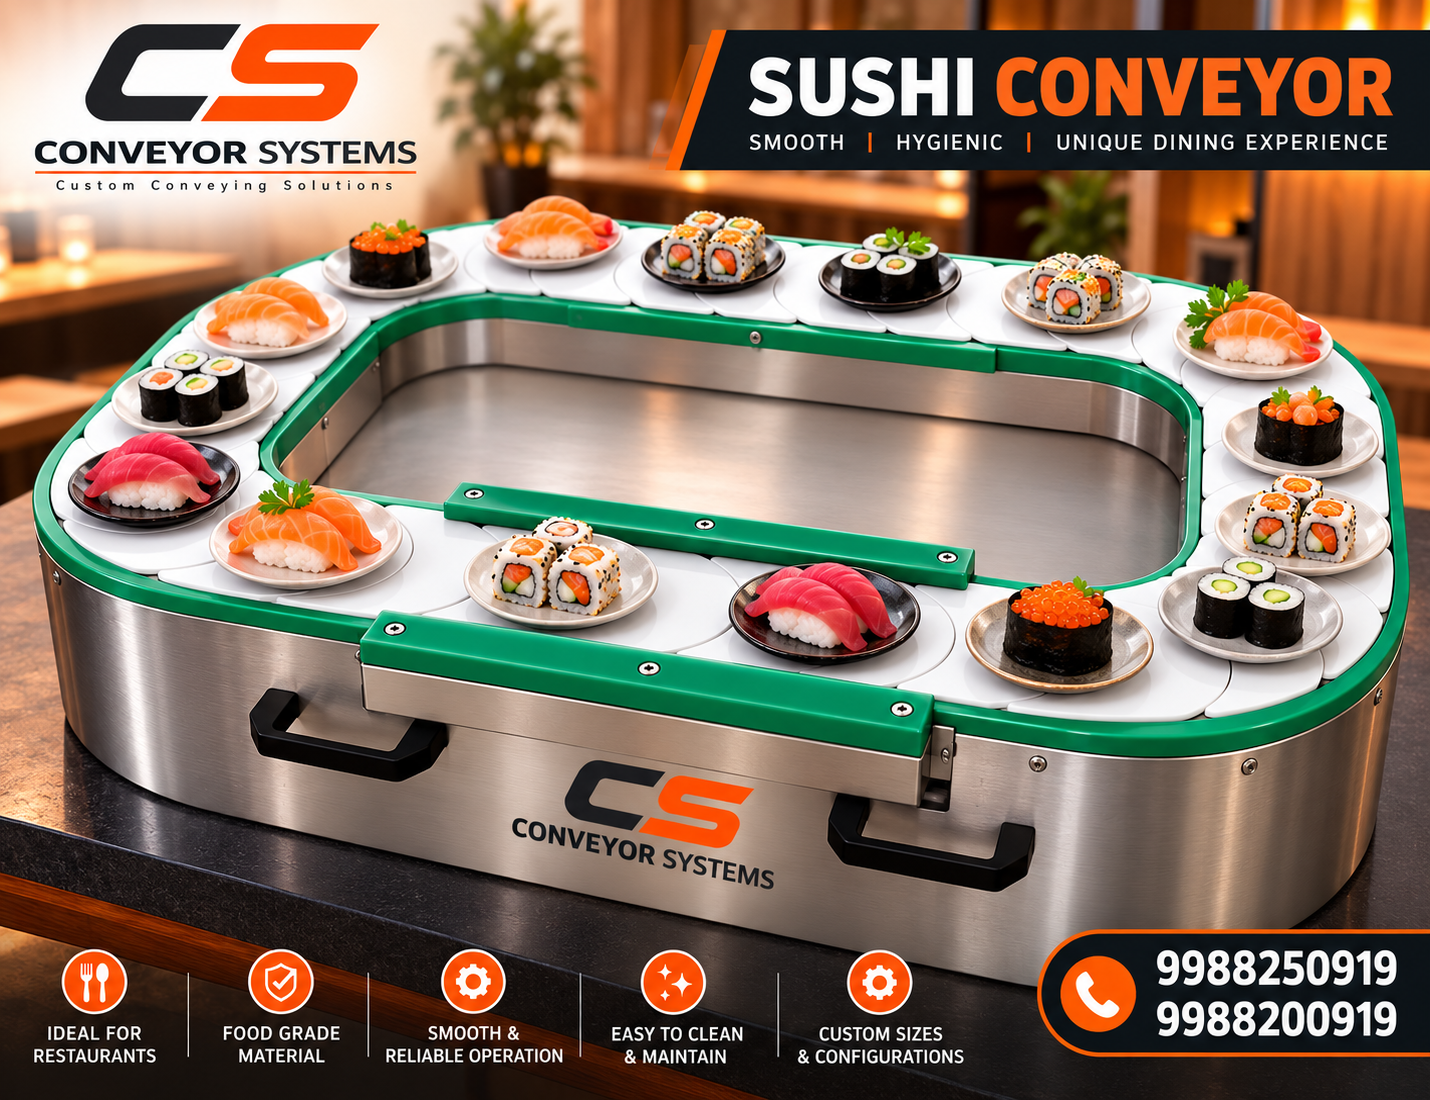
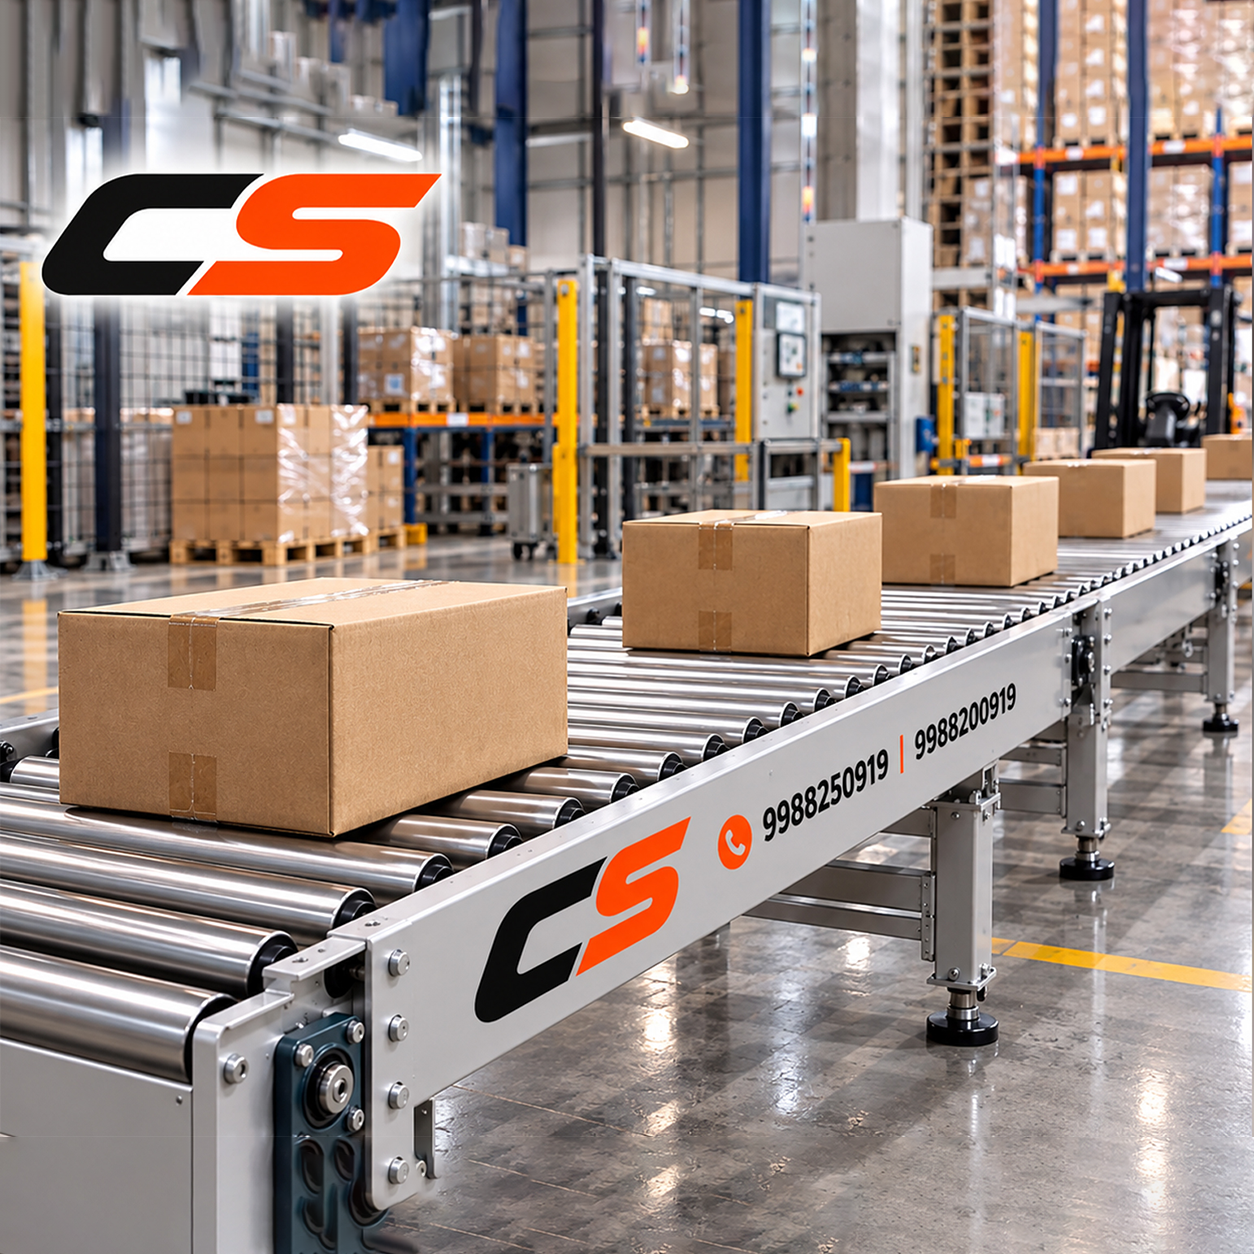
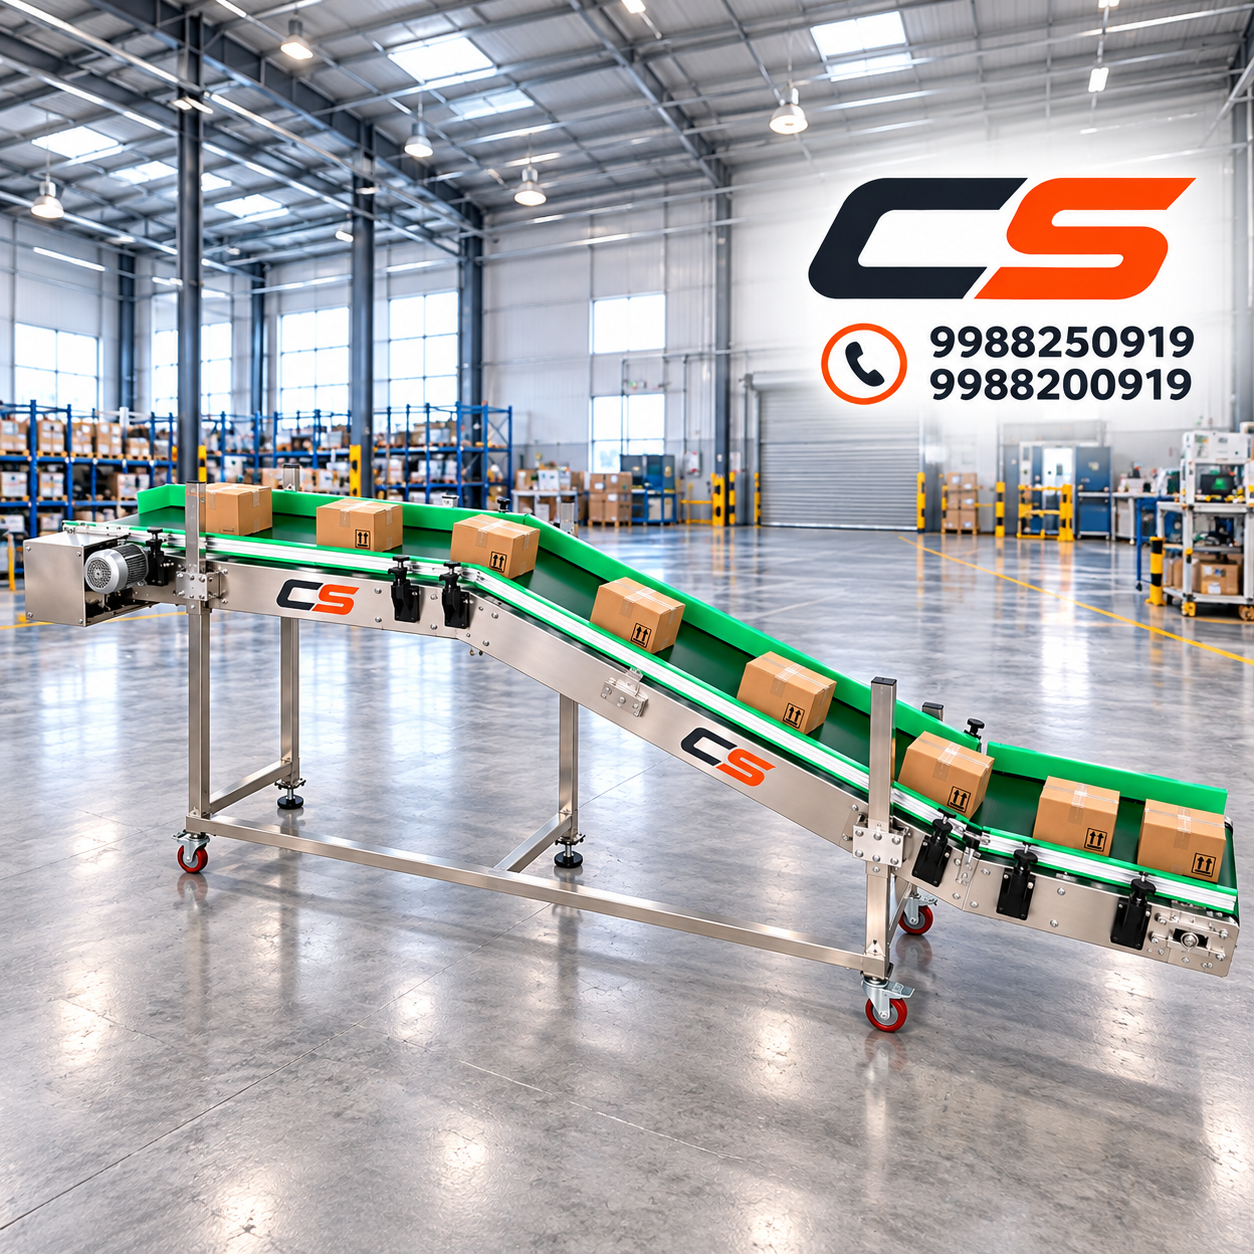
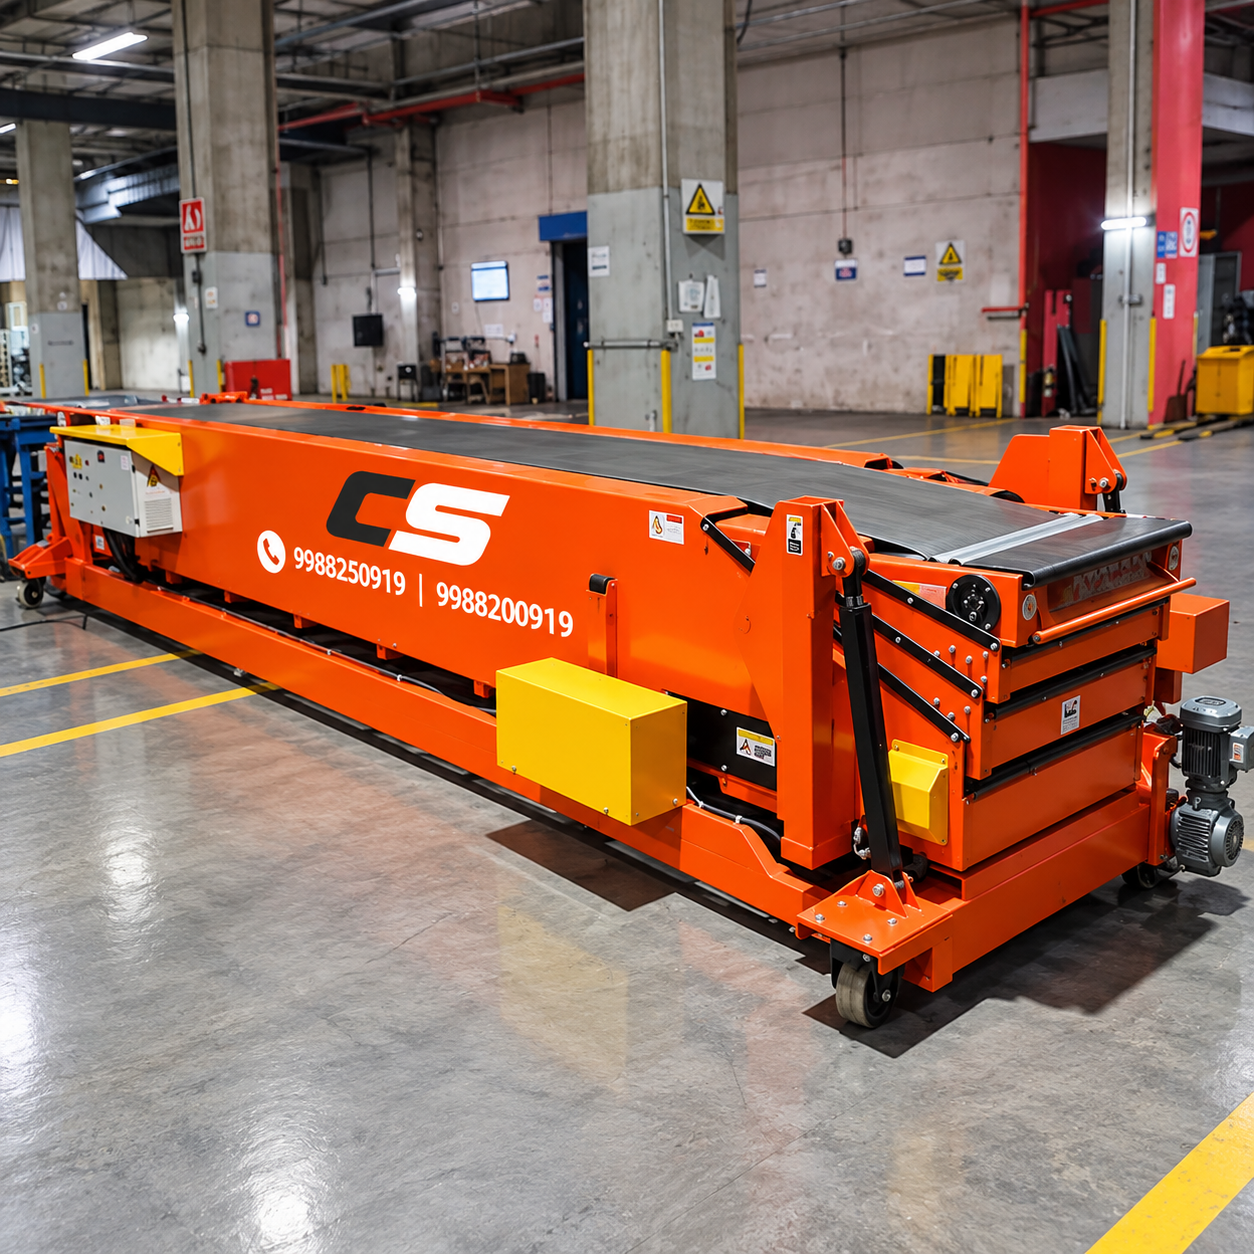
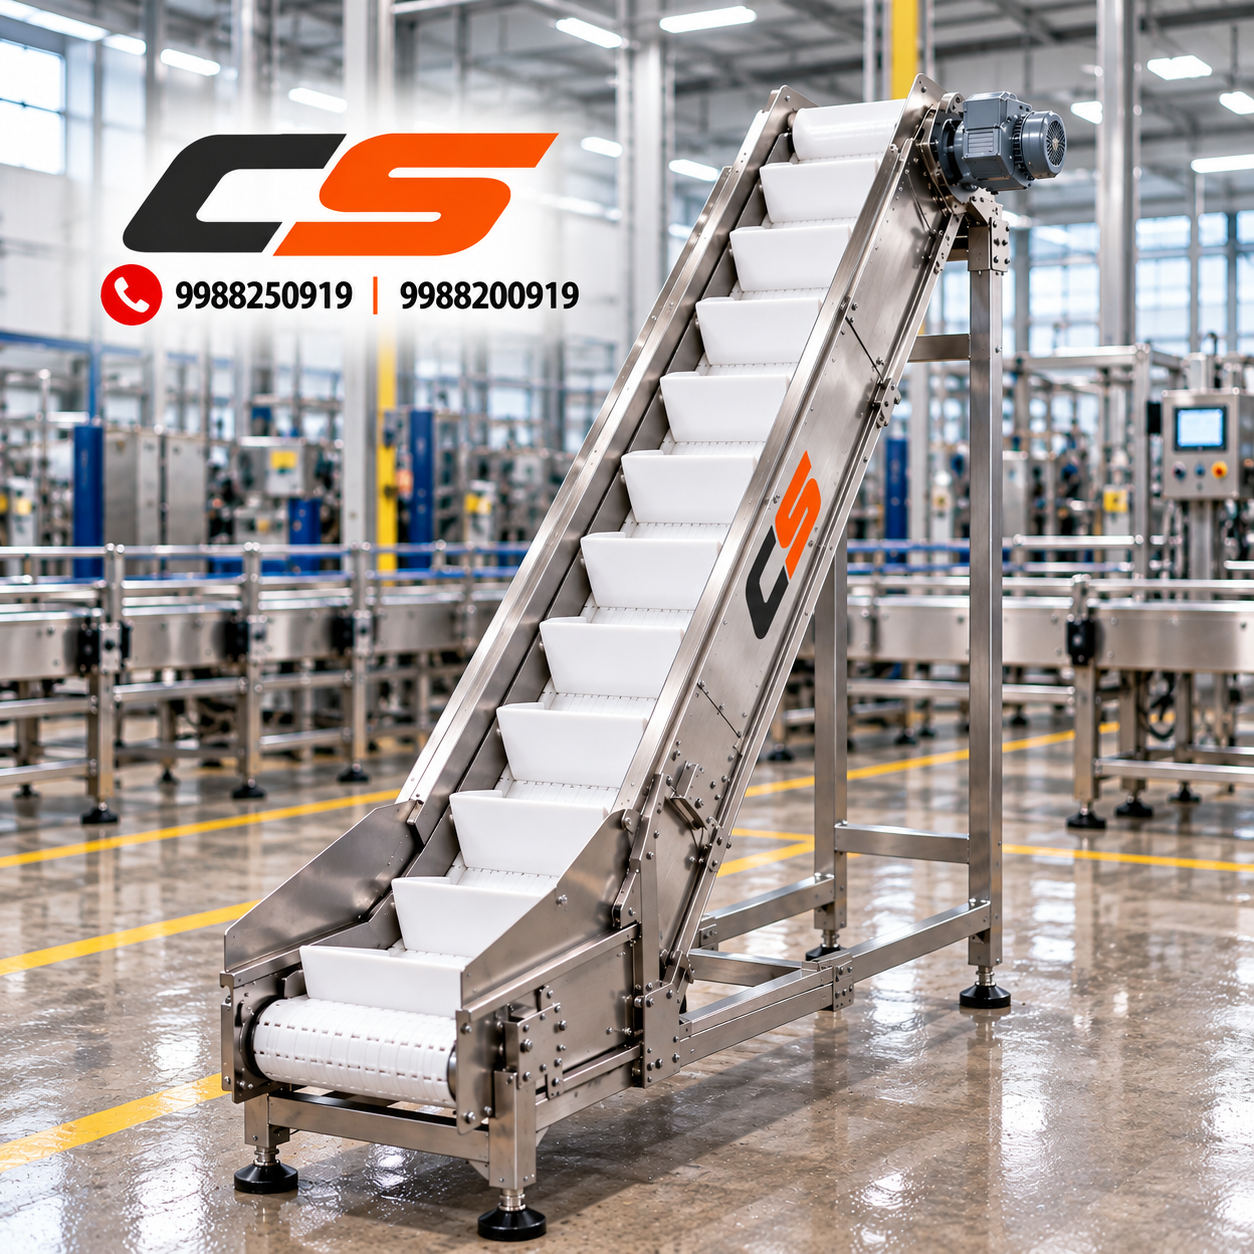
-
Our Mission
To provide reliable, high-quality conveyor systems that improve material handling,
enhance operational efficiency, and deliver customized solutions that meet the
specific requirements of every customer. -
Our Vision
To become a trusted leader in conveyor and material handling solutions by
delivering innovative, durable, and cost-effective systems that support modern
industries and long-term business growth. -
Our Values
We are committed to quality, reliability, innovation, customer satisfaction,
safety, and professional service. We believe in building long-term relationships
through dependable products and consistent support.
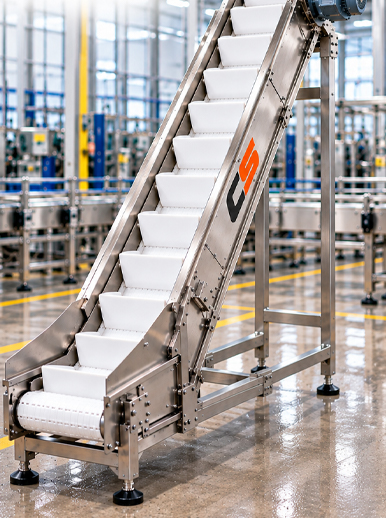
Reliable Conveyor
System Solutions
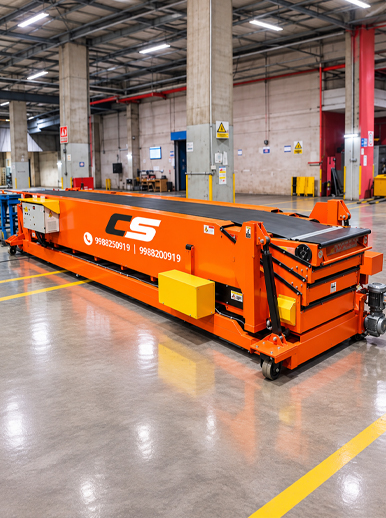
Reliable Conveyor Solutions for Modern Industries
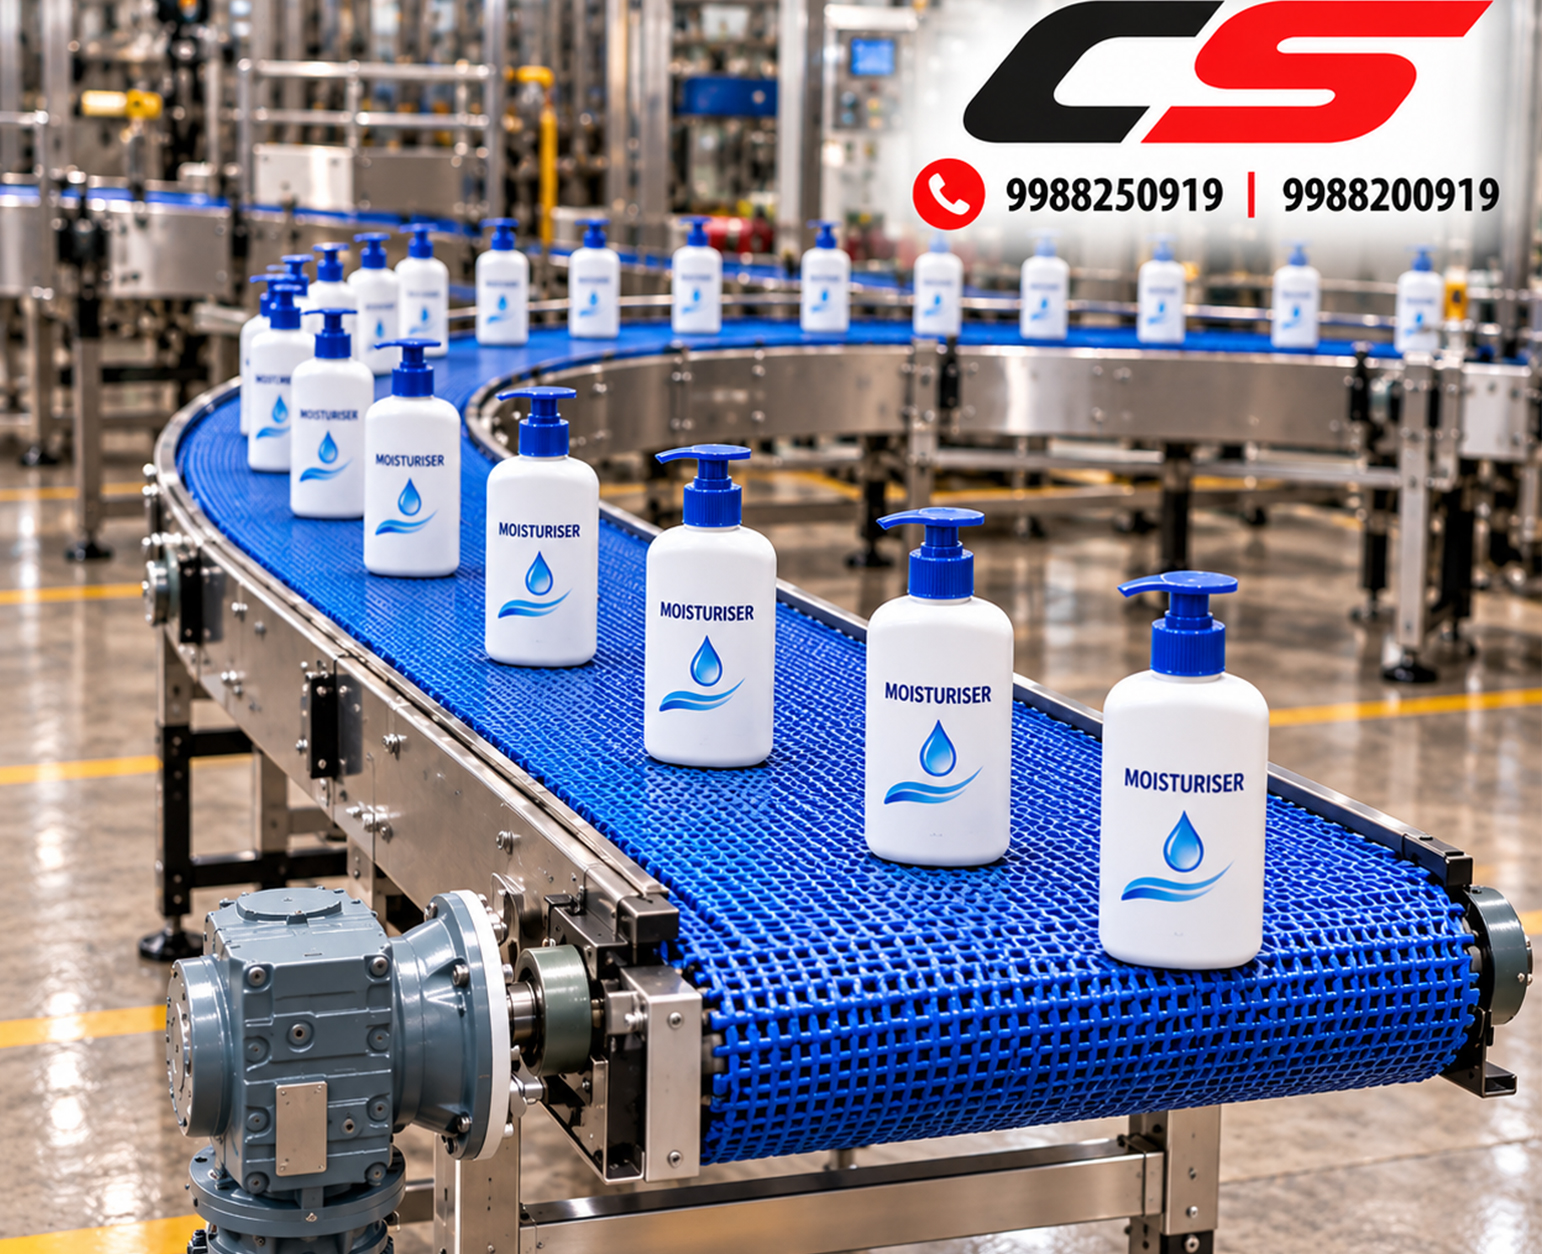
Conveyor Systems is a trusted manufacturer and supplier of Belt Conveyors, Modular Conveyors, Cleated Conveyors, Bend Conveyors and customized material handling solutions. We provide efficient conveyor systems designed to meet the diverse requirements of manufacturing, packaging, logistics, warehousing, and other industrial applications.
With a focus on quality, durability, and performance, our conveyor systems are engineered using reliable components and robust construction. We work closely with our customers to understand their application requirements and deliver customized, cost-effective solutions that ensure smooth material movement, improved productivity, easy maintenance, and long-term operational reliability.
From Concept to Complete Conveyor System Installation
Requirement Analysis & Consultation
Conveyor Design & Manufacturing
Quality Testing & Performance Inspection
Installation, Commissioning & Support
Conveyor Systems Video Gallery
Explore our conveyor systems, machines and industrial solutions through our video gallery.
Pvc Cleated incline Conveyor belt
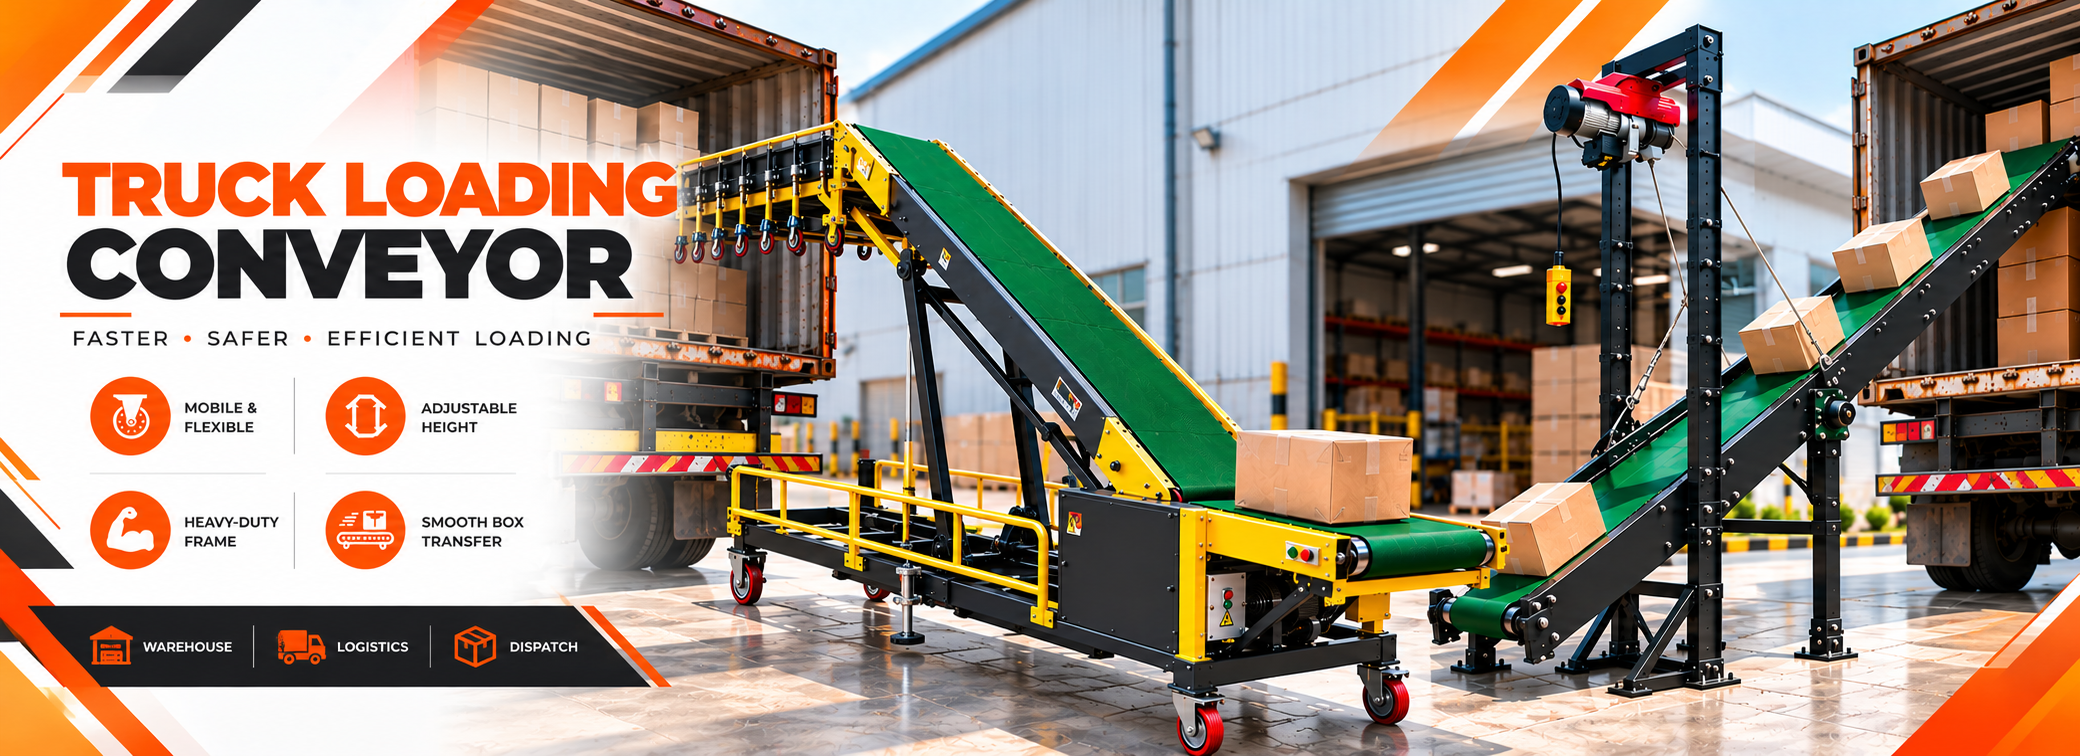
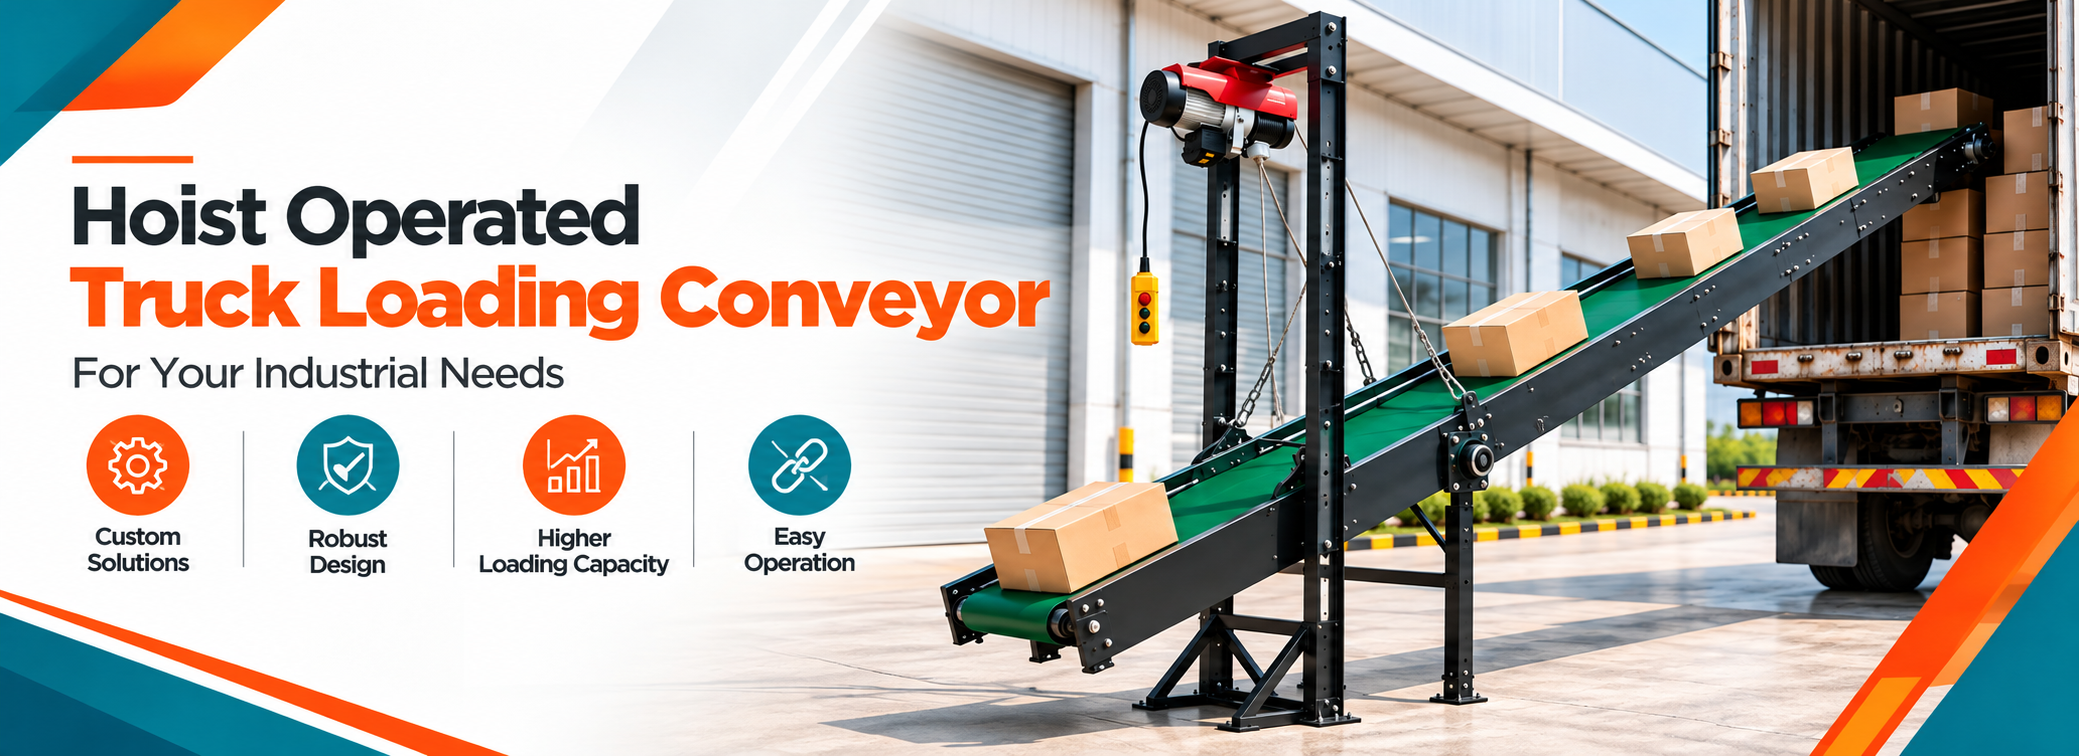
manually operated truck loading conveyor
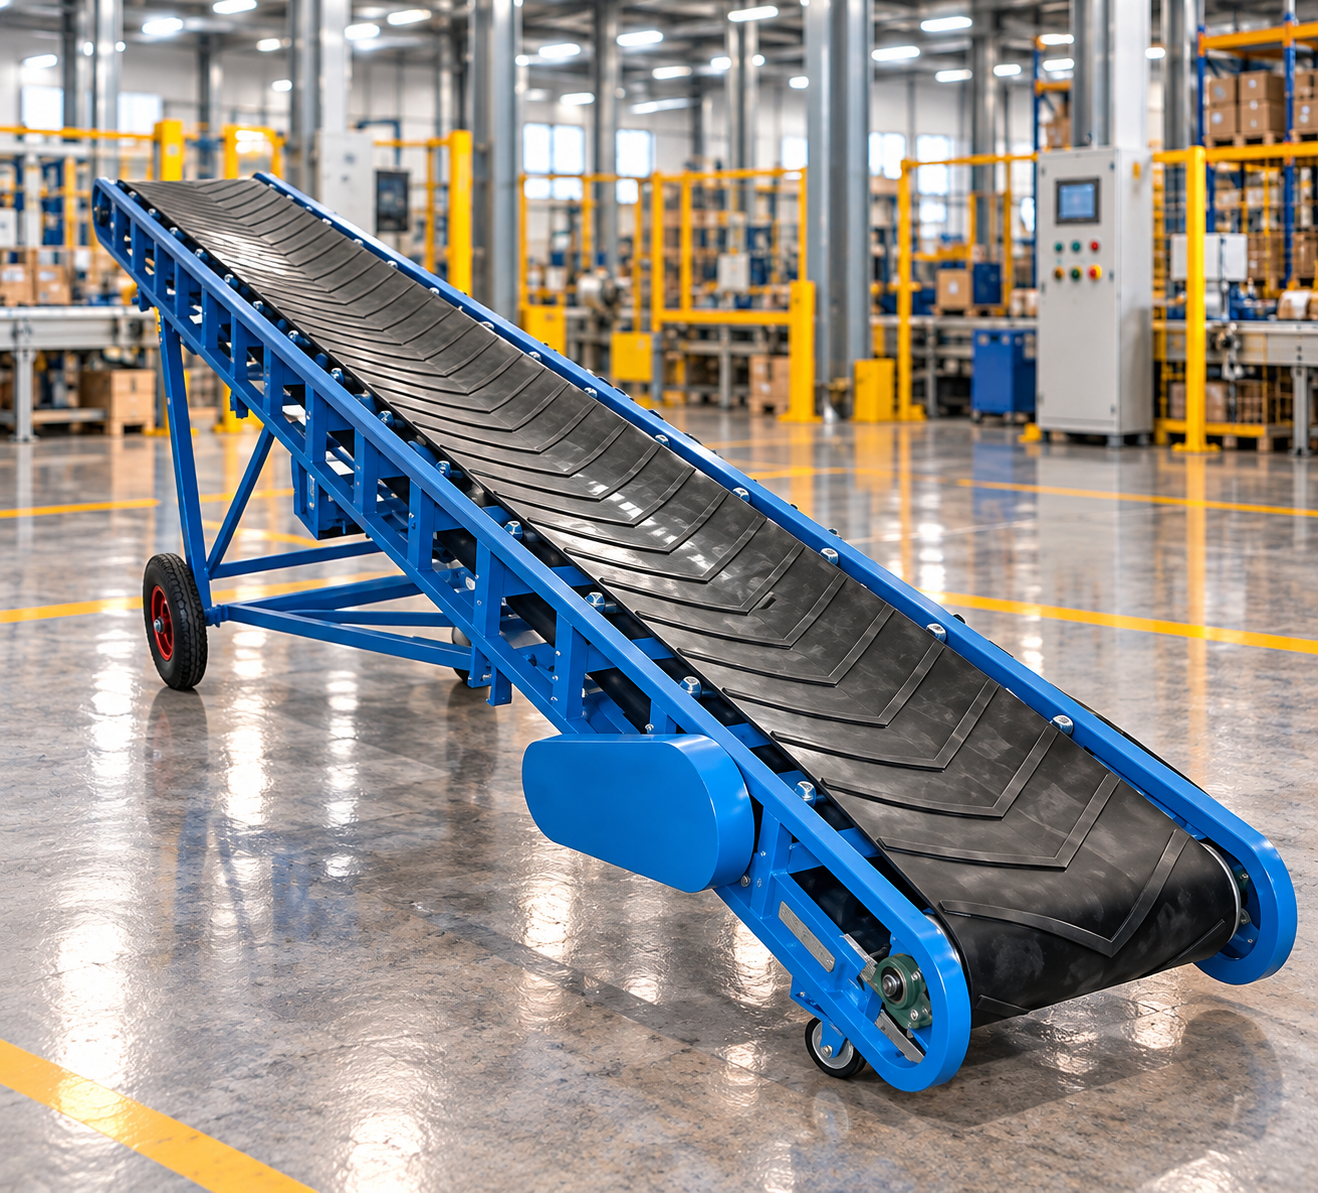
Industrial Inclined Conveyor in Warehouse
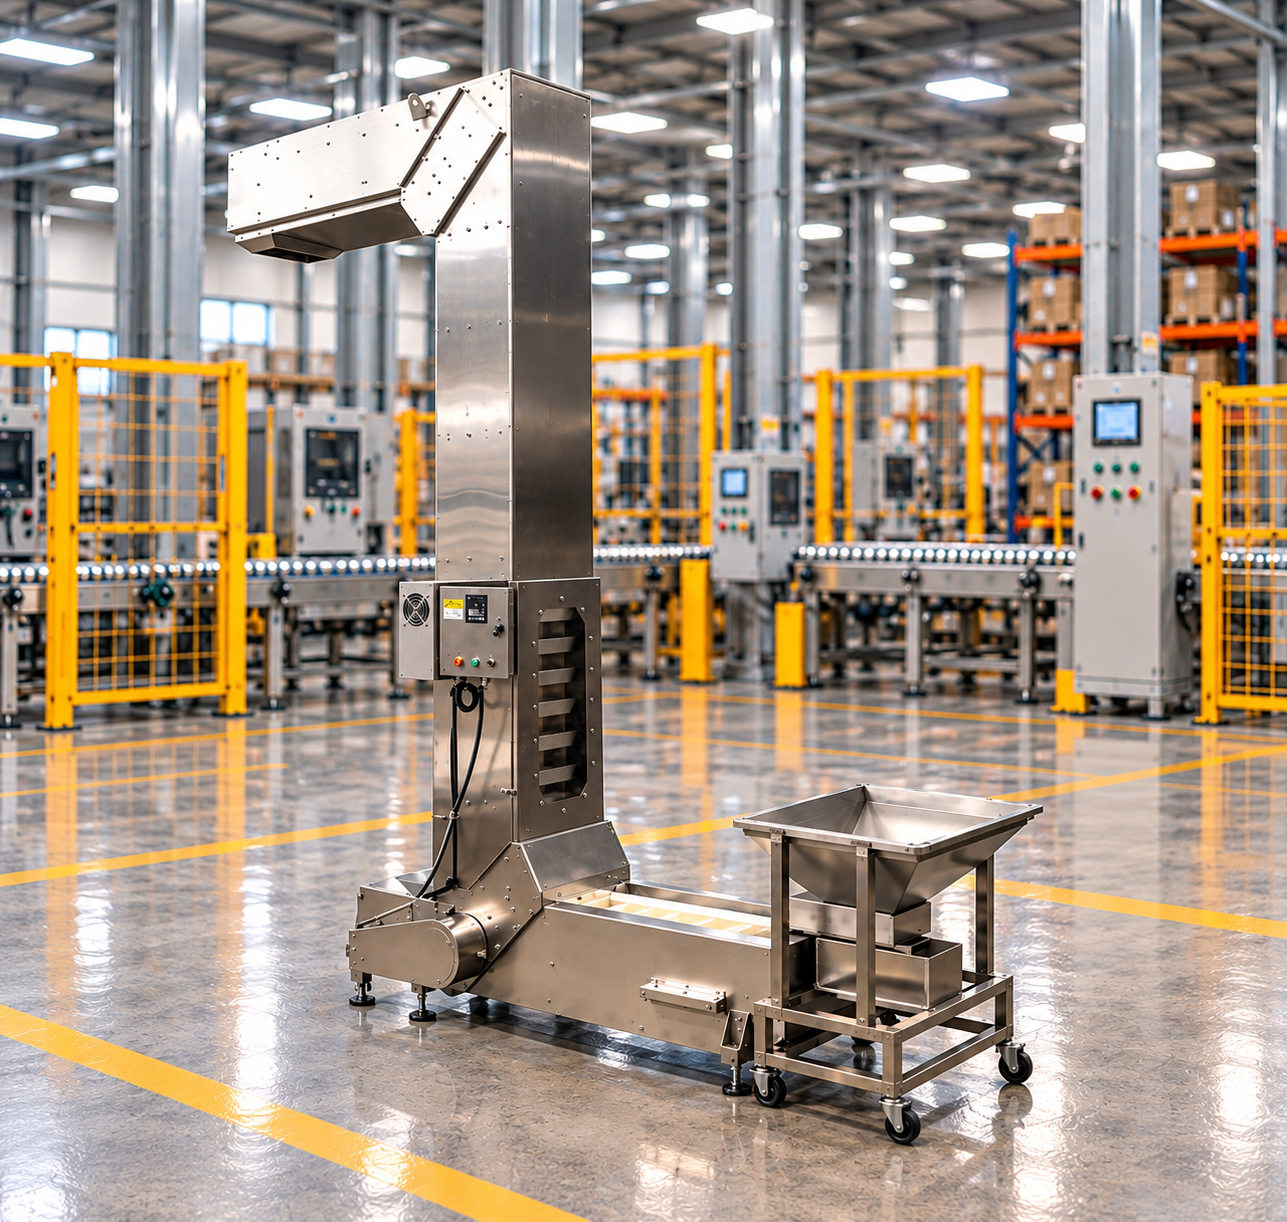
Elevator Cleated Modular Conveyor
Fixed truck loading conveyor
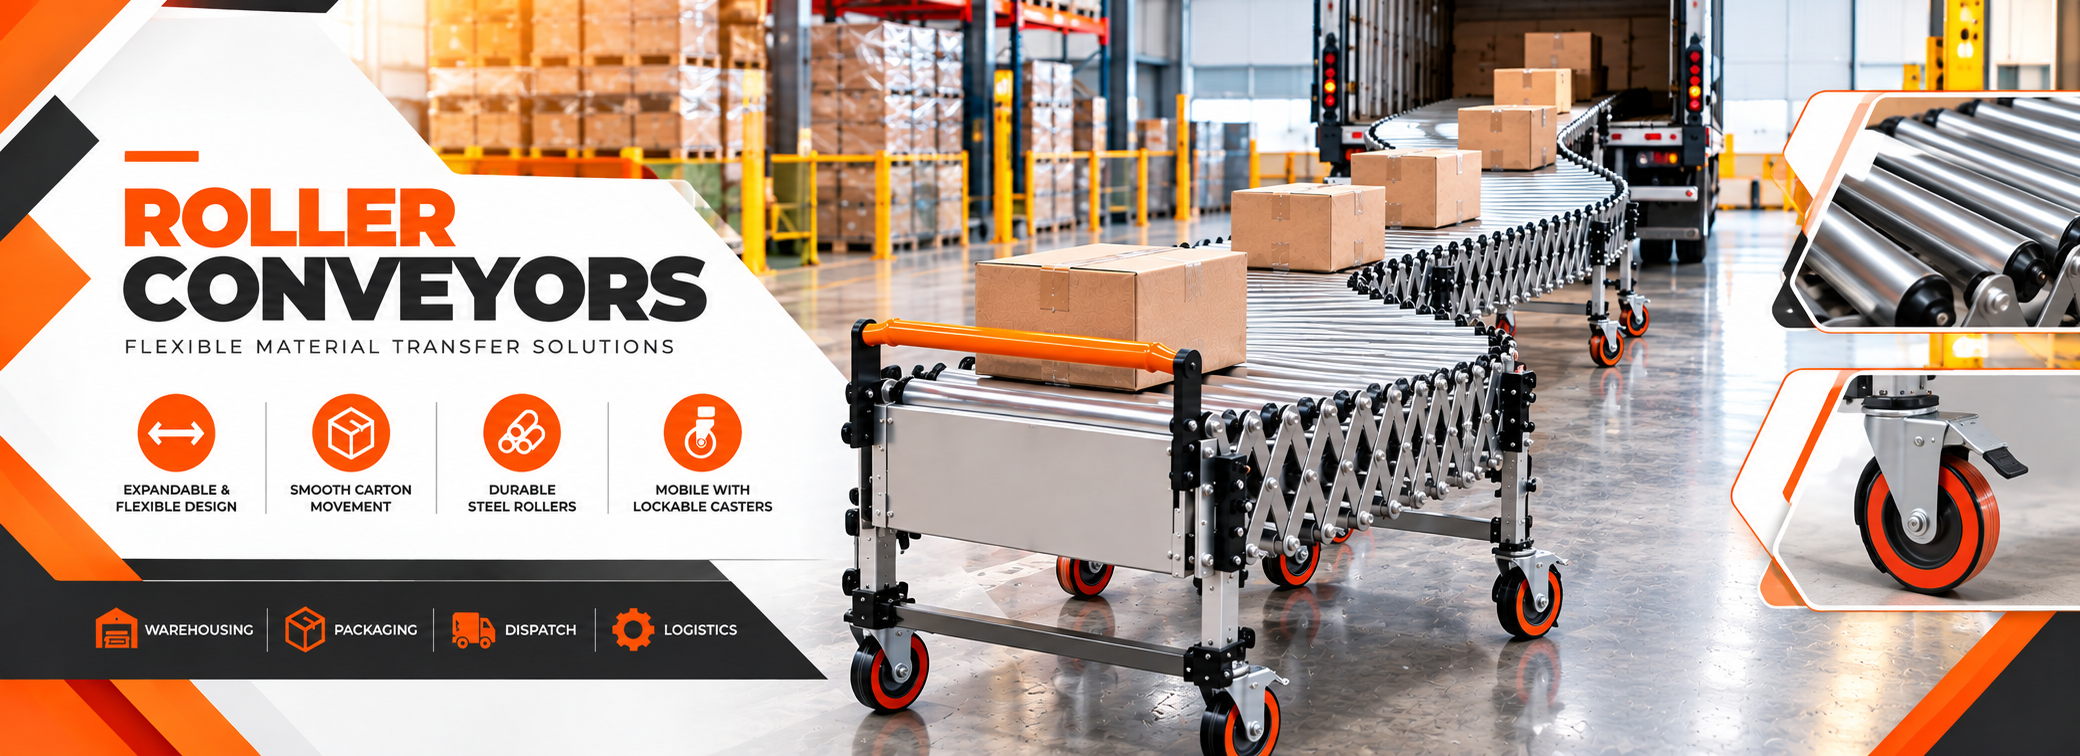
Extendable roller integrated hydraulic
U shaped roller conveyor
Extendable roller integrated hydraulic
Straight Acetate Conveyor Belt
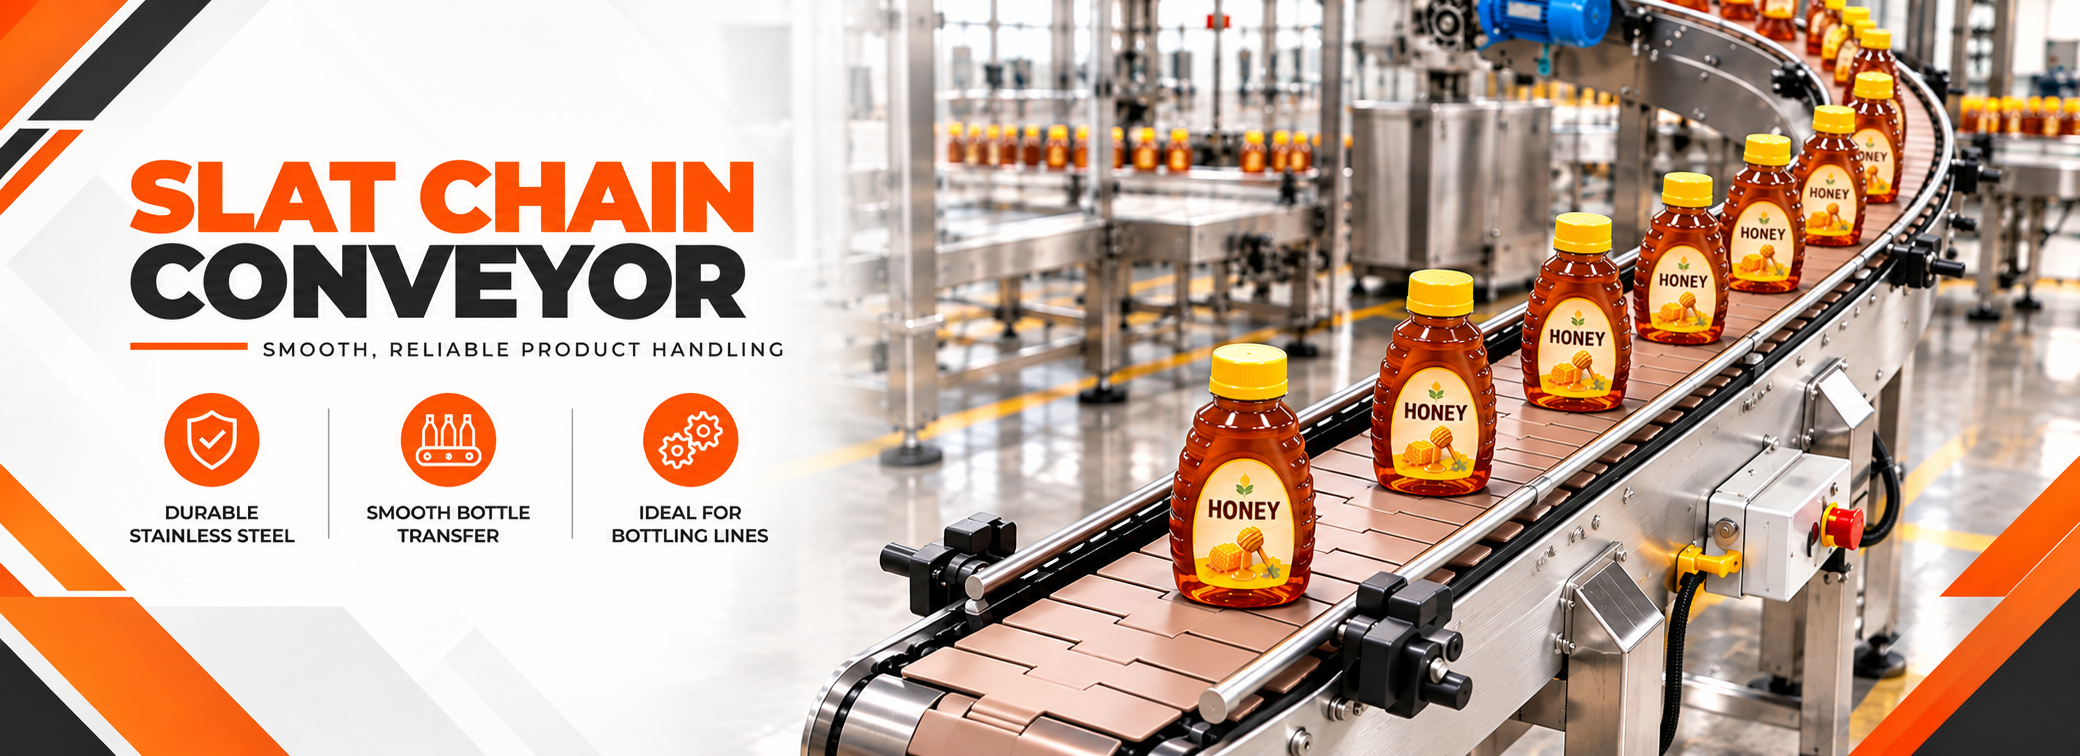
SS Curved Slat Chain
OUR CAPABILITIES
0+
Years of
Industry Experience
0+
Conveyor Systems
Delivered
0+
Successful
Projects
100%
Quality &
Customer Satisfaction
Conveyor System Solutions
Conveyor Systems
- Belt Conveyor Systems
- Industrial Belt Conveyors
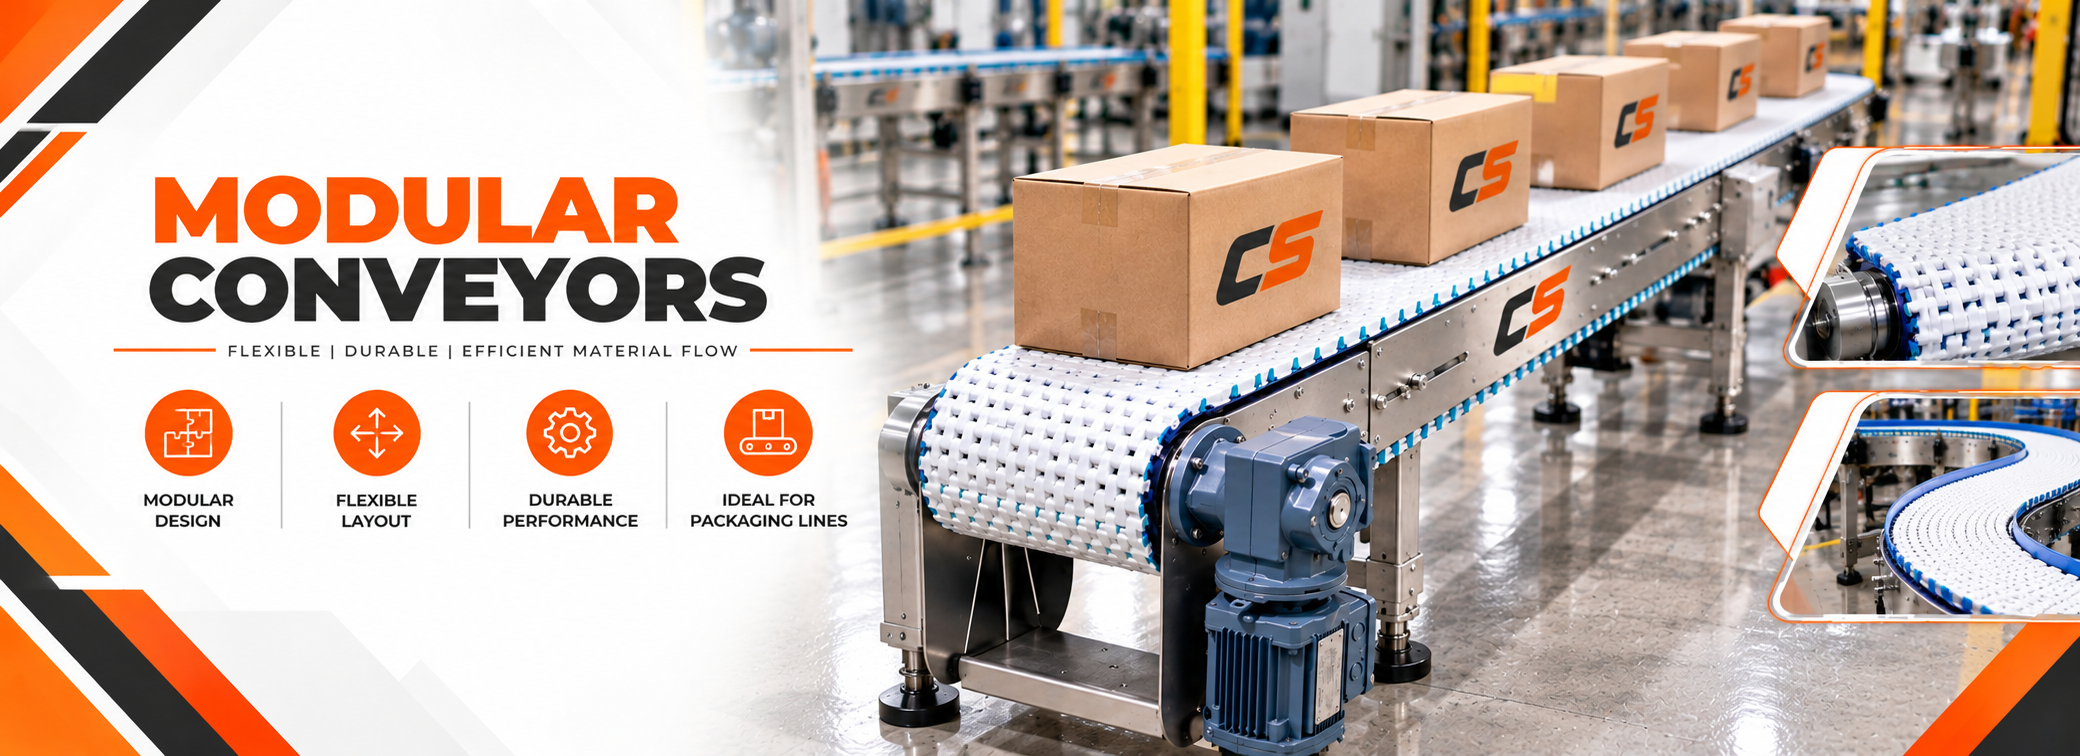
- Modular Belt Conveyors
- Cleated Belt Conveyors
- Inclined Conveyor Systems
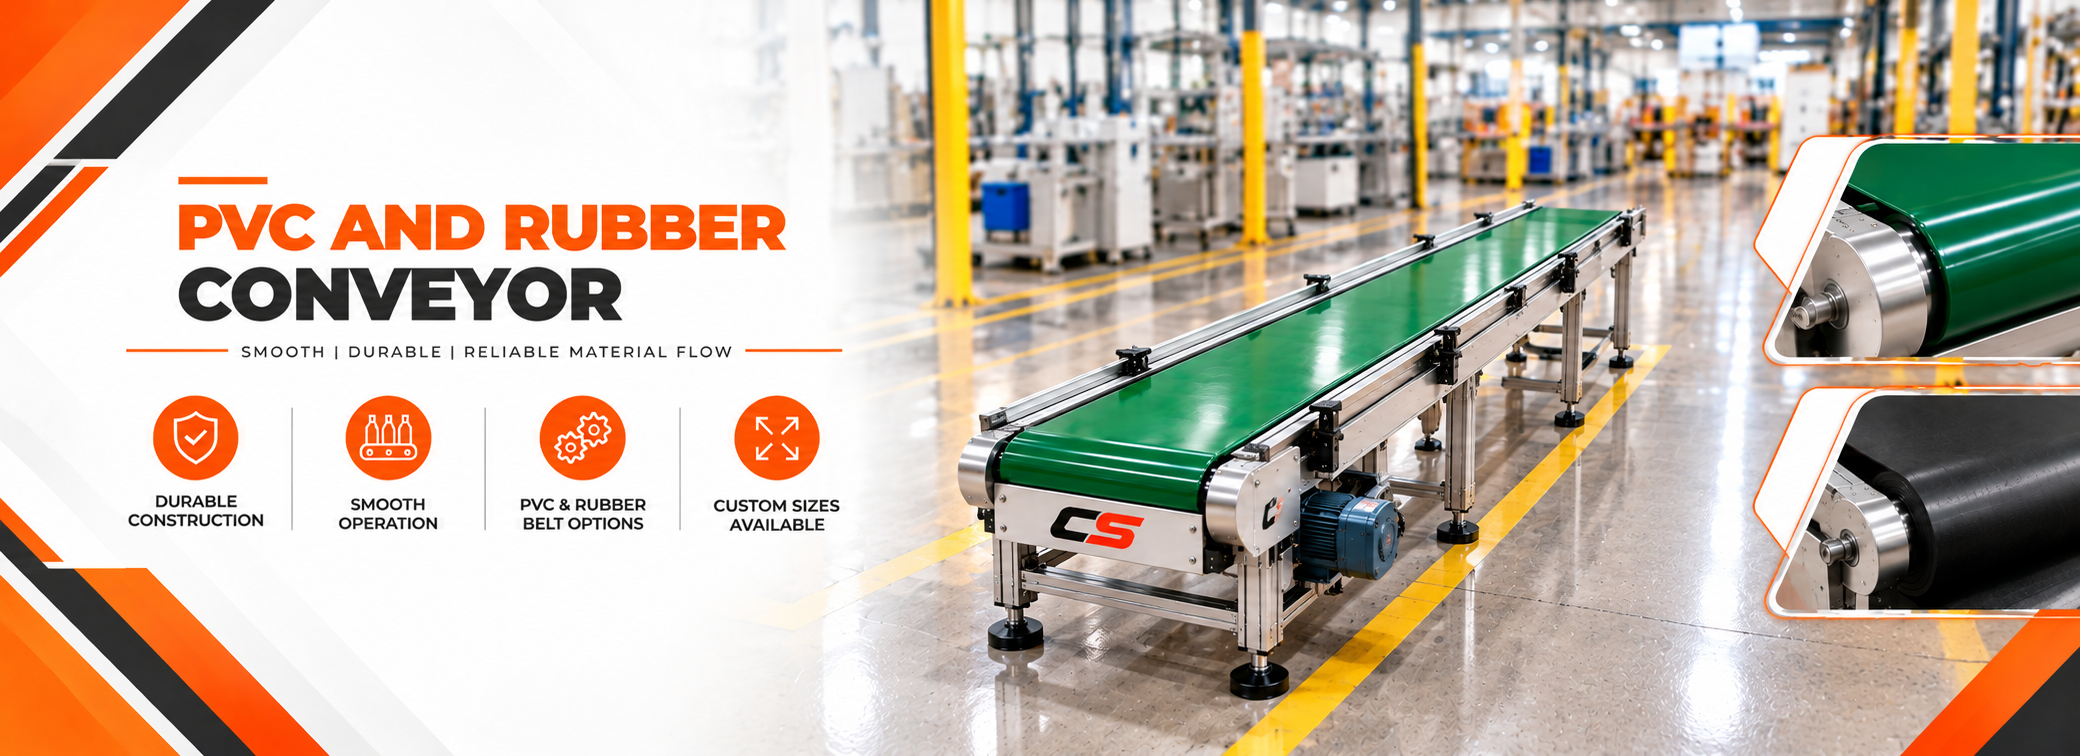
- Flat Belt Conveyors
- Roller Conveyor Systems
- Heavy Duty Conveyors
Customized Material Handling
- Curved & Bend Conveyors
- Food & Packaging Conveyors
- Assembly Line Conveyors
- Warehouse Material Handling Systems
- Industrial Transfer Conveyors
- Customized Conveyor Solutions
- Conveyor Automation Solutions
- Material Handling Equipment
Reliable Conveyor Systems & Material Handling Solutions
At Conveyor Systems, we provide dependable and customized conveyor solutions designed to improve material movement, production efficiency, and workplace productivity. Our systems are engineered with quality components, robust construction, and attention to detail to ensure smooth and reliable performance across various industrial applications.
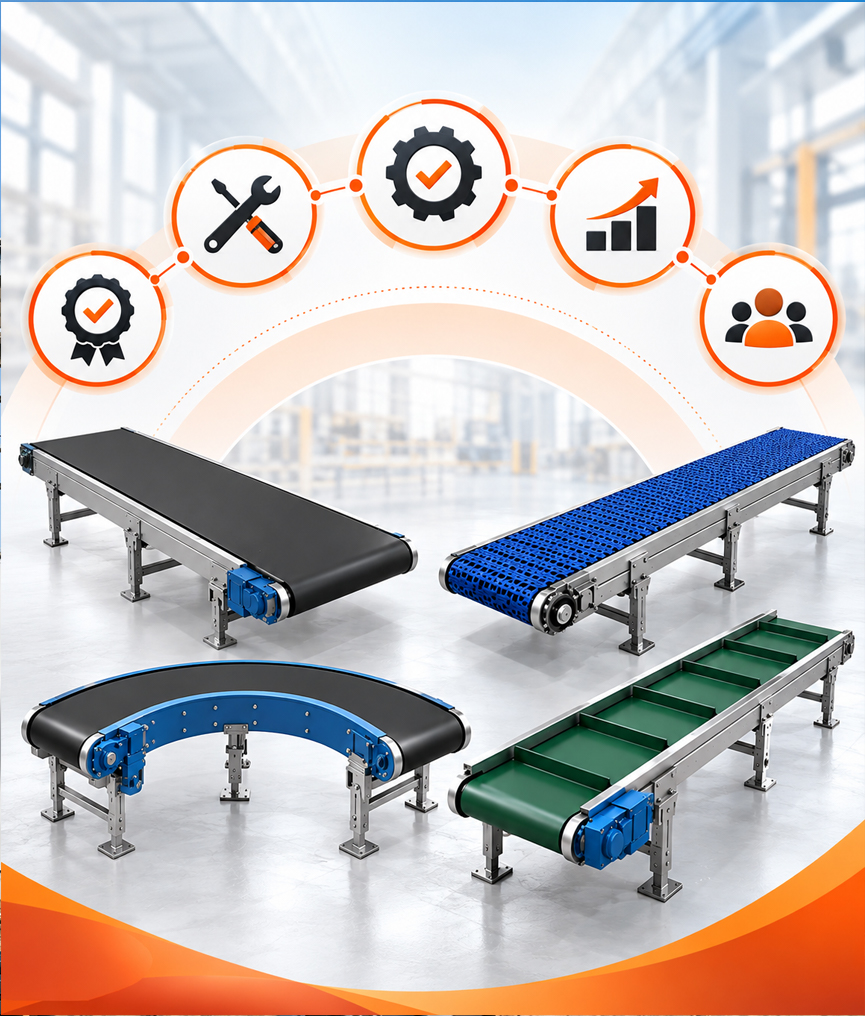
Efficient Conveyor Solutions for Modern Industries
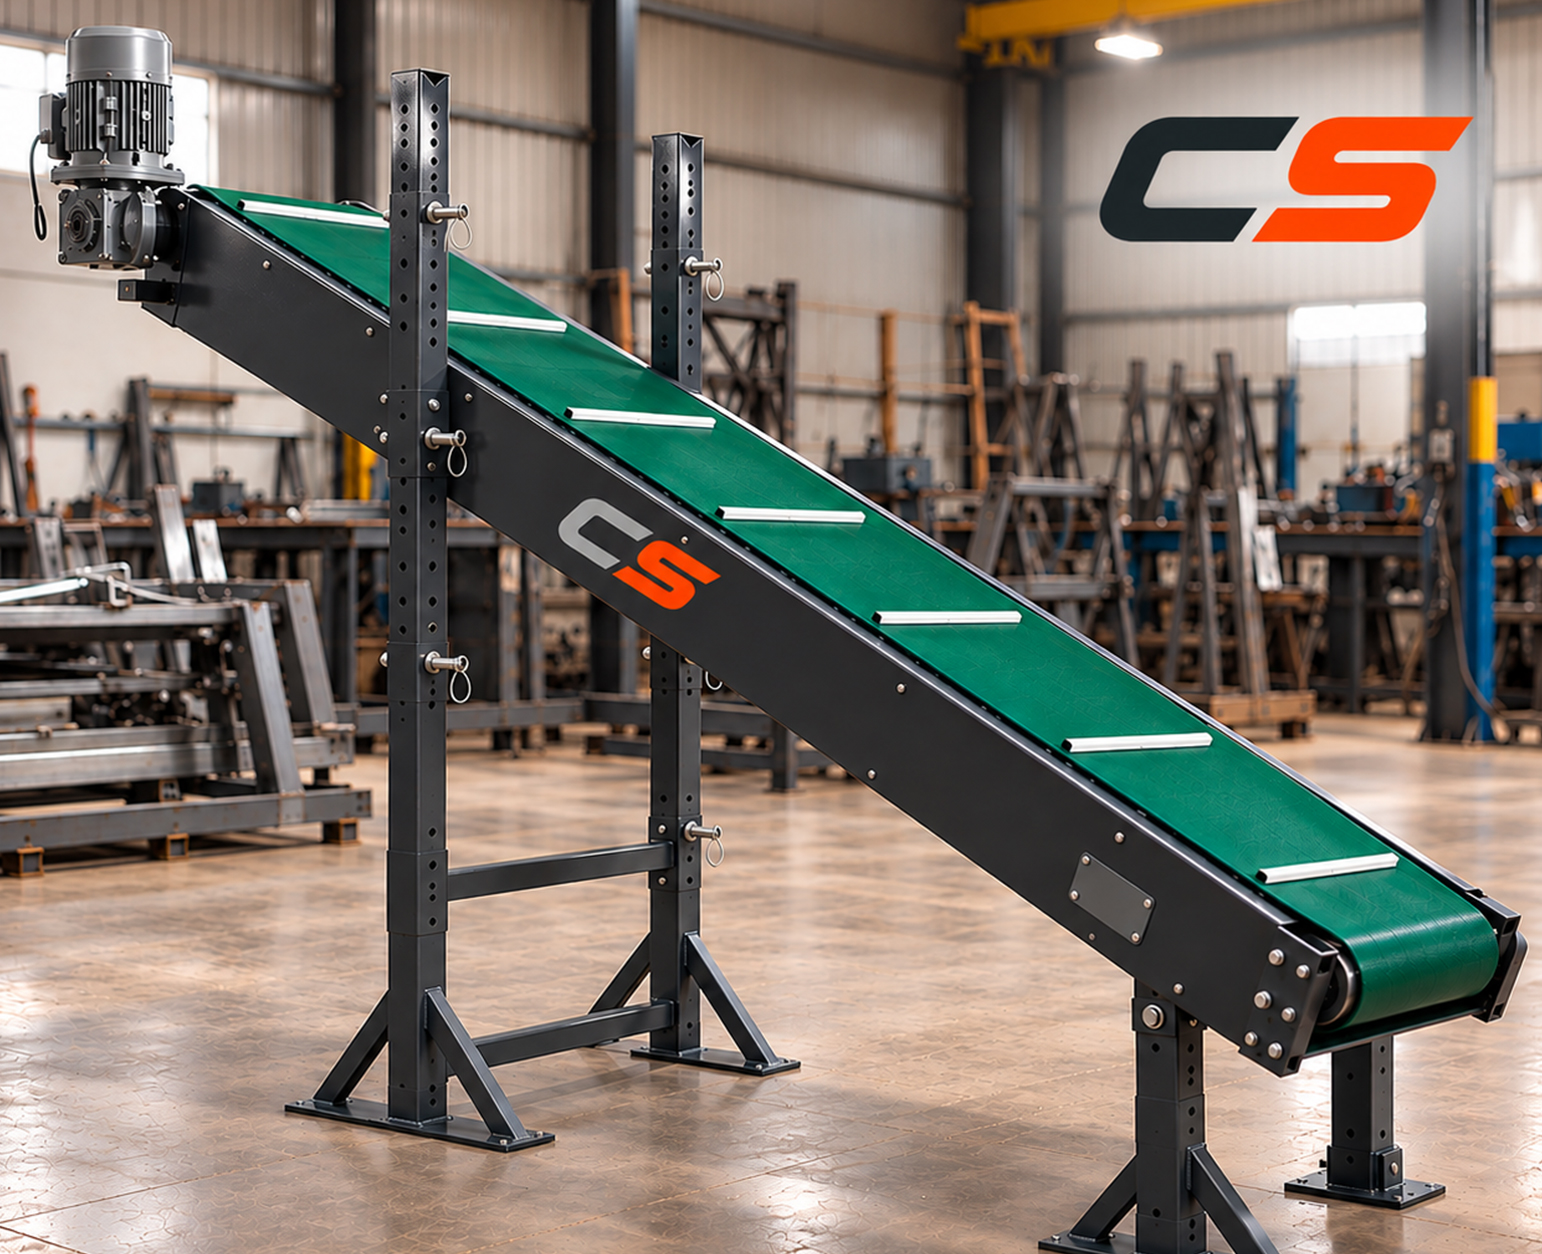
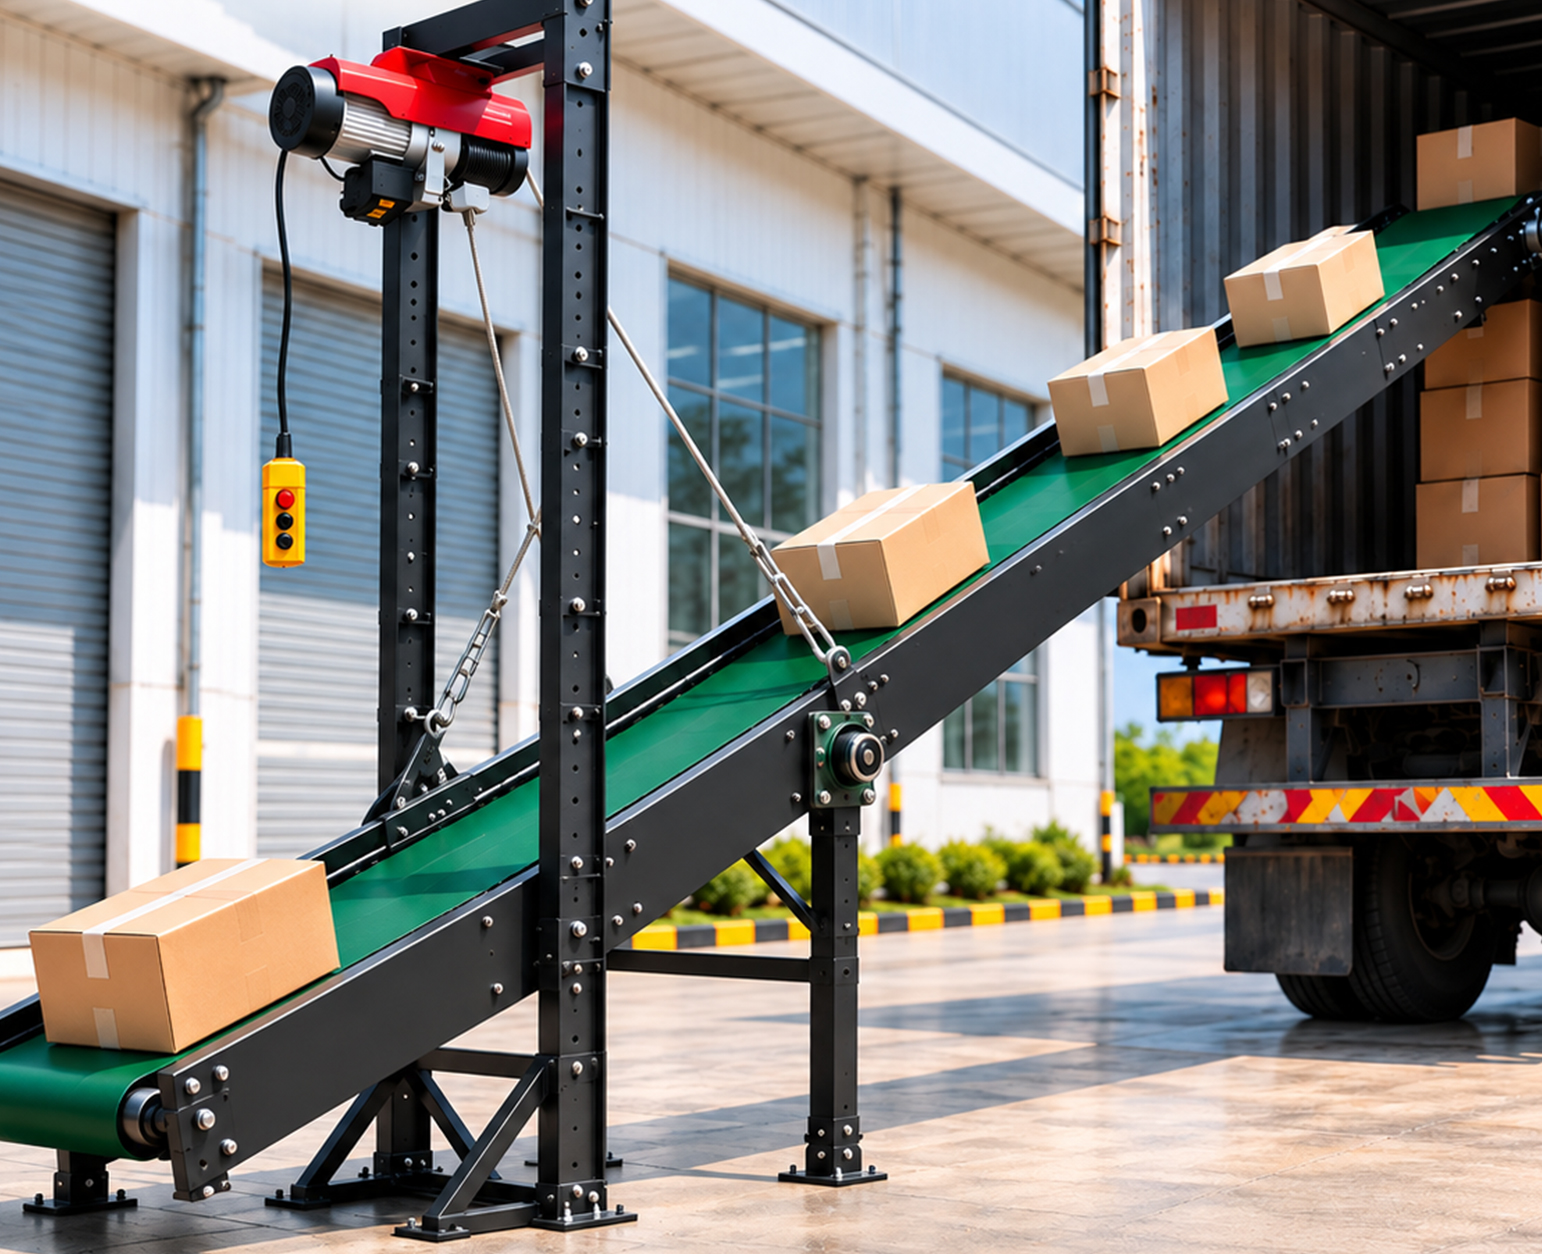
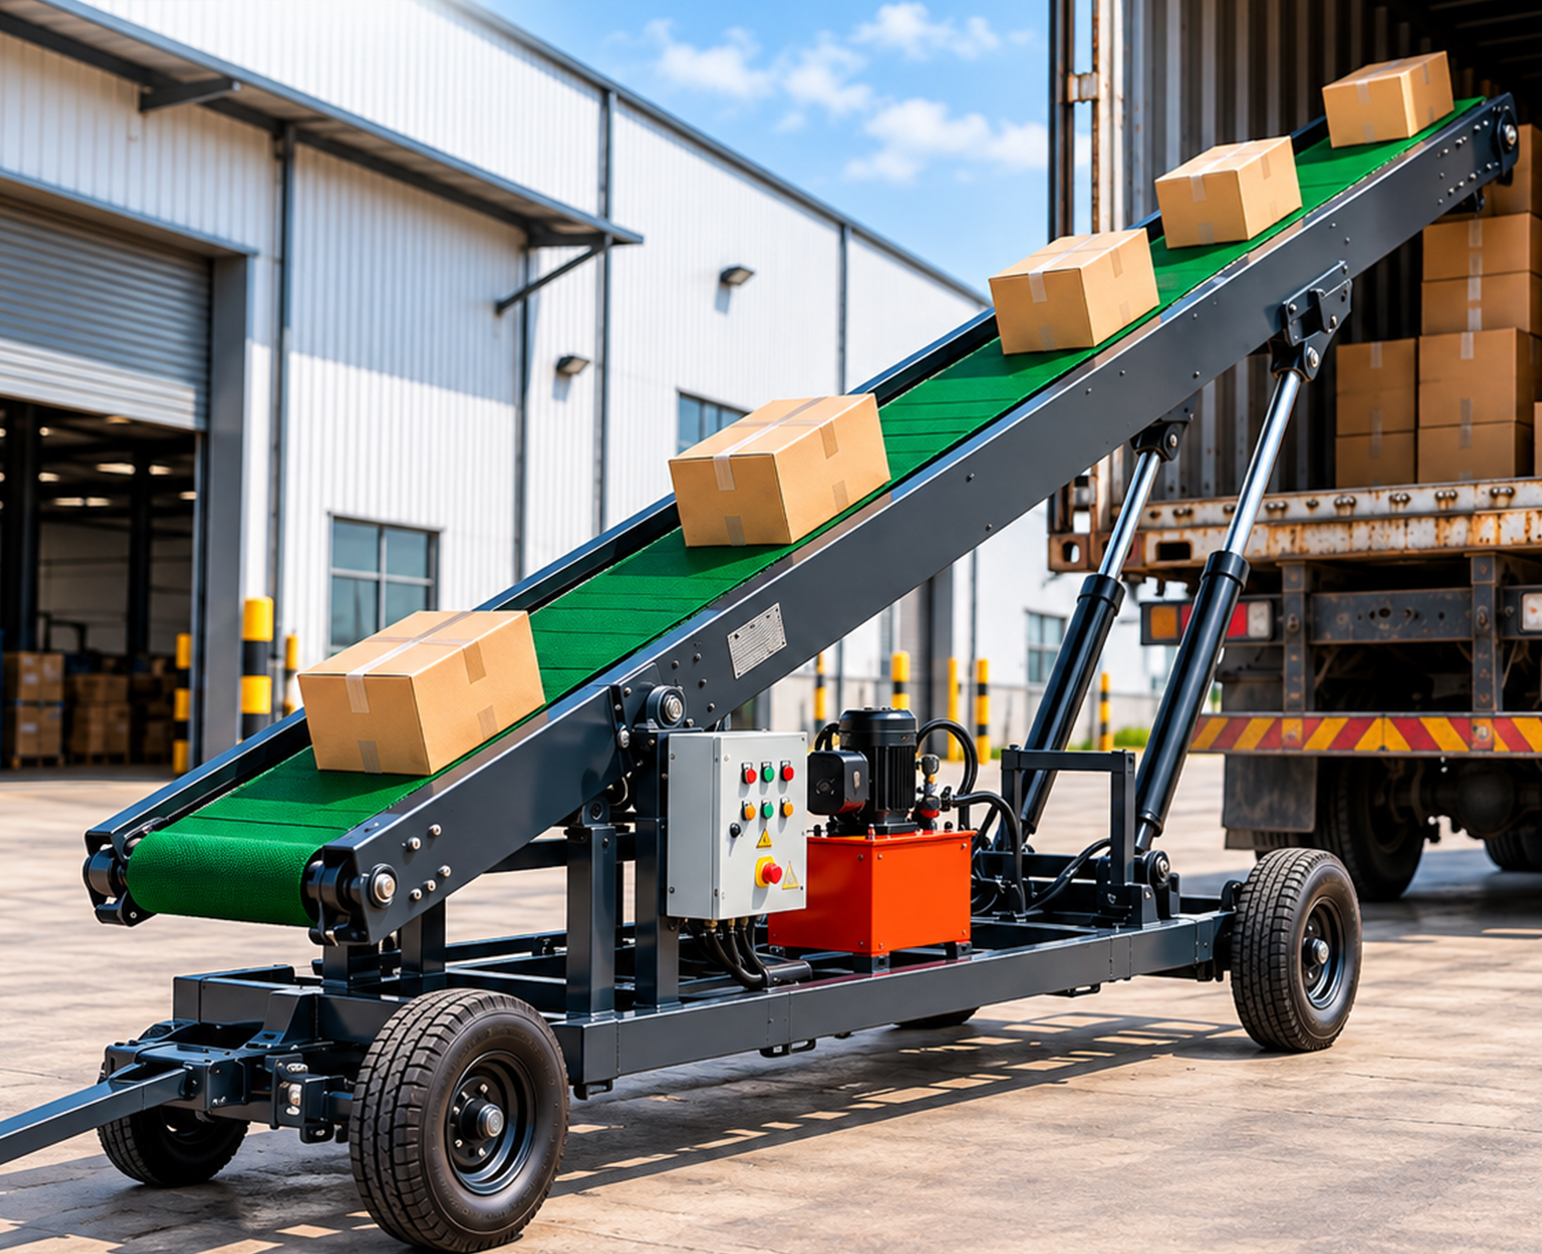
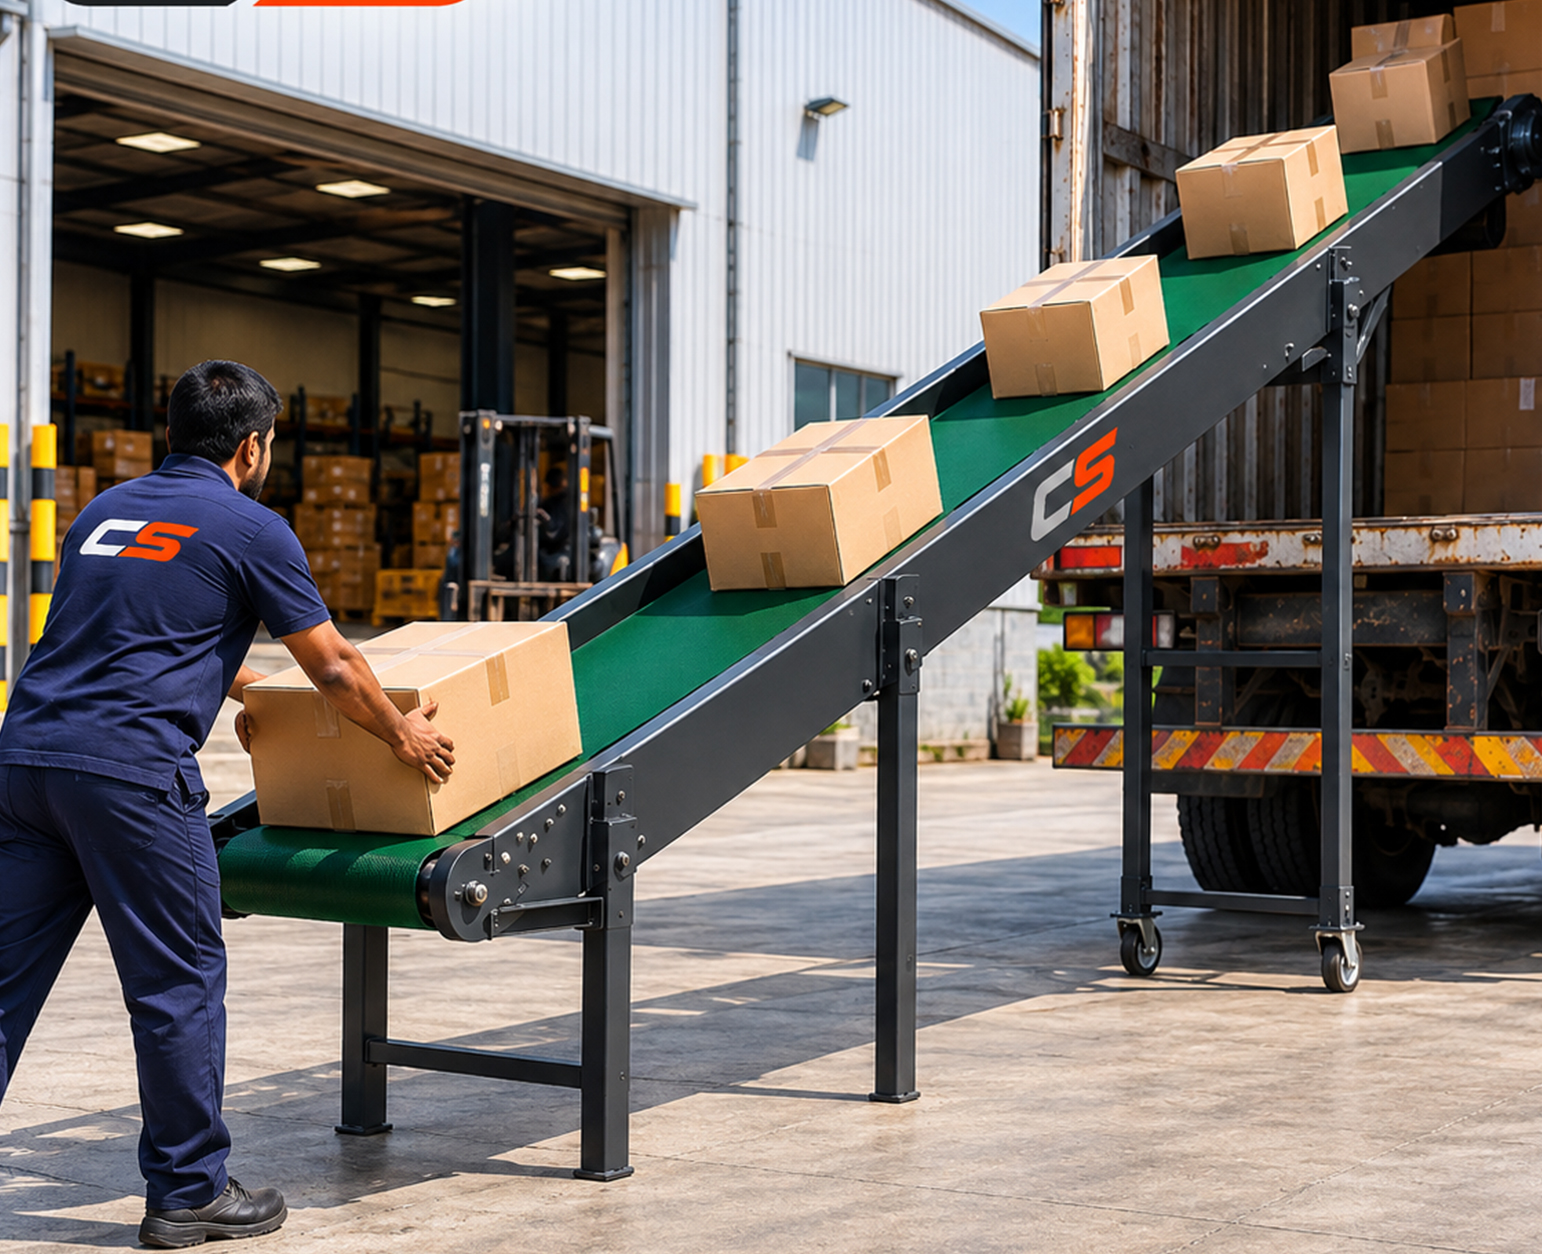
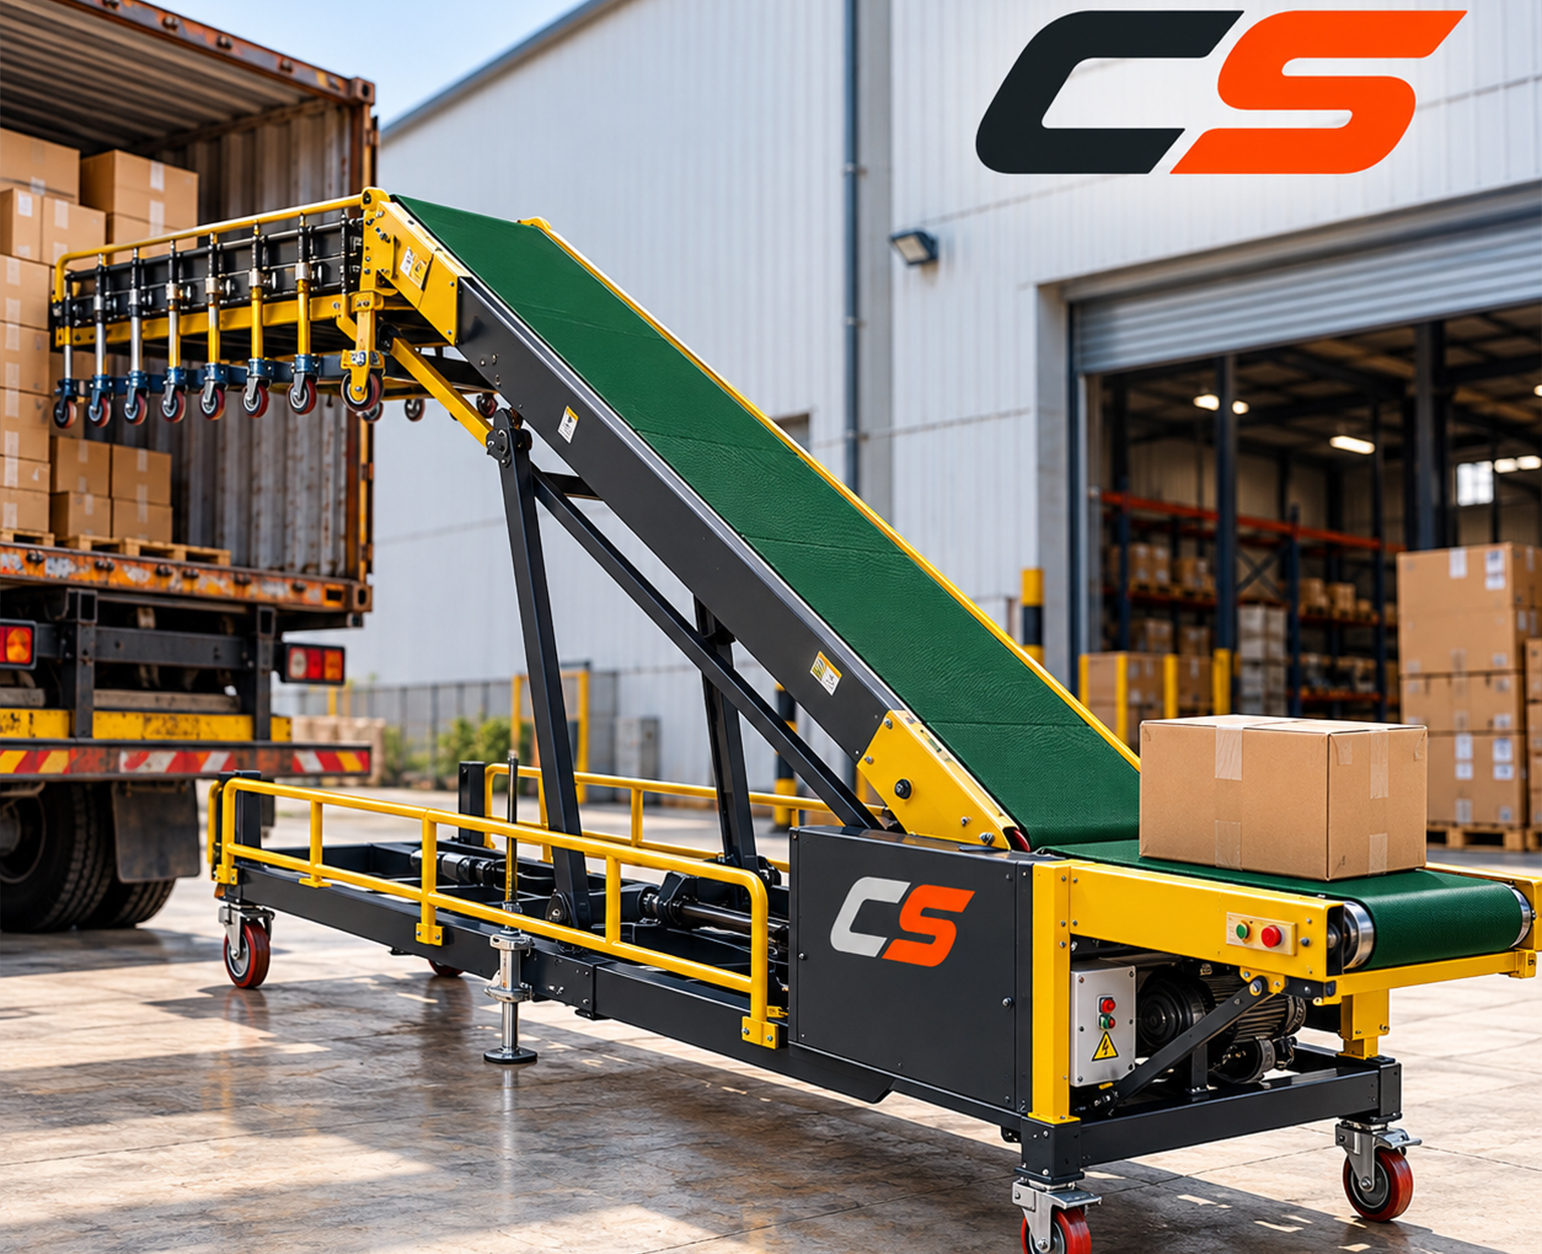
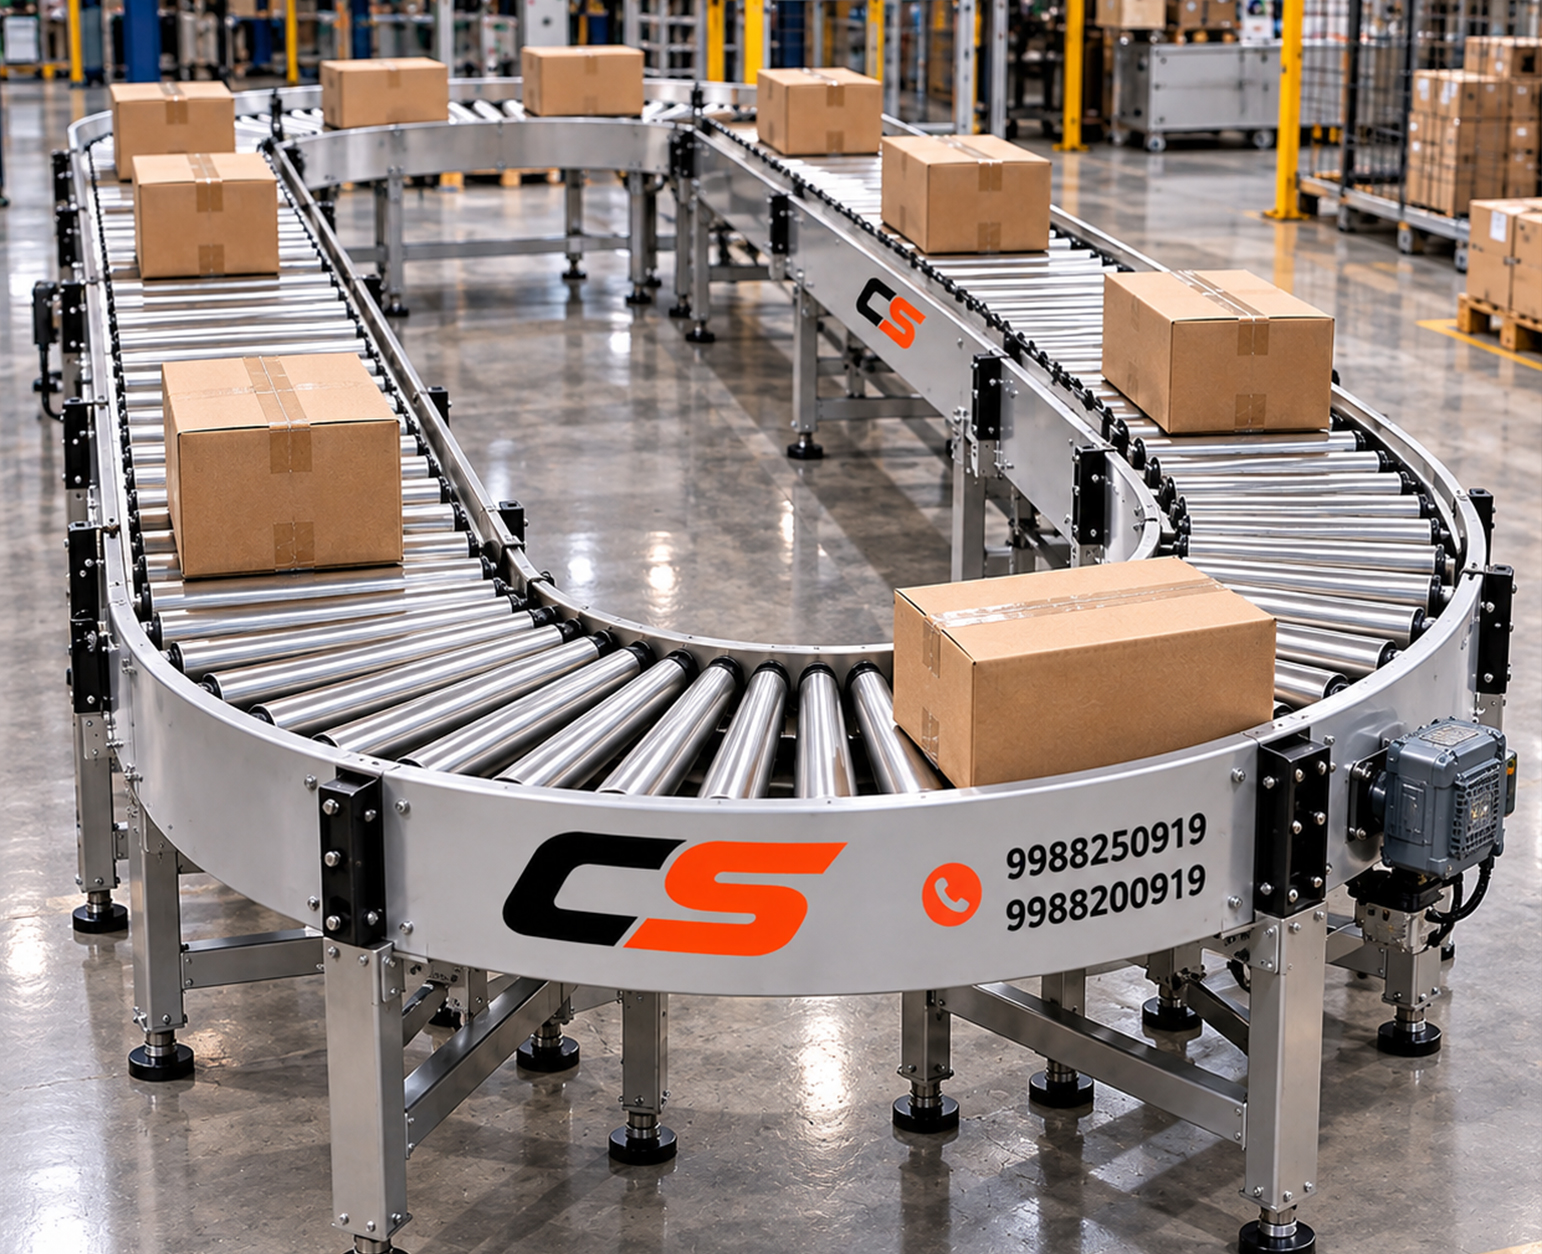
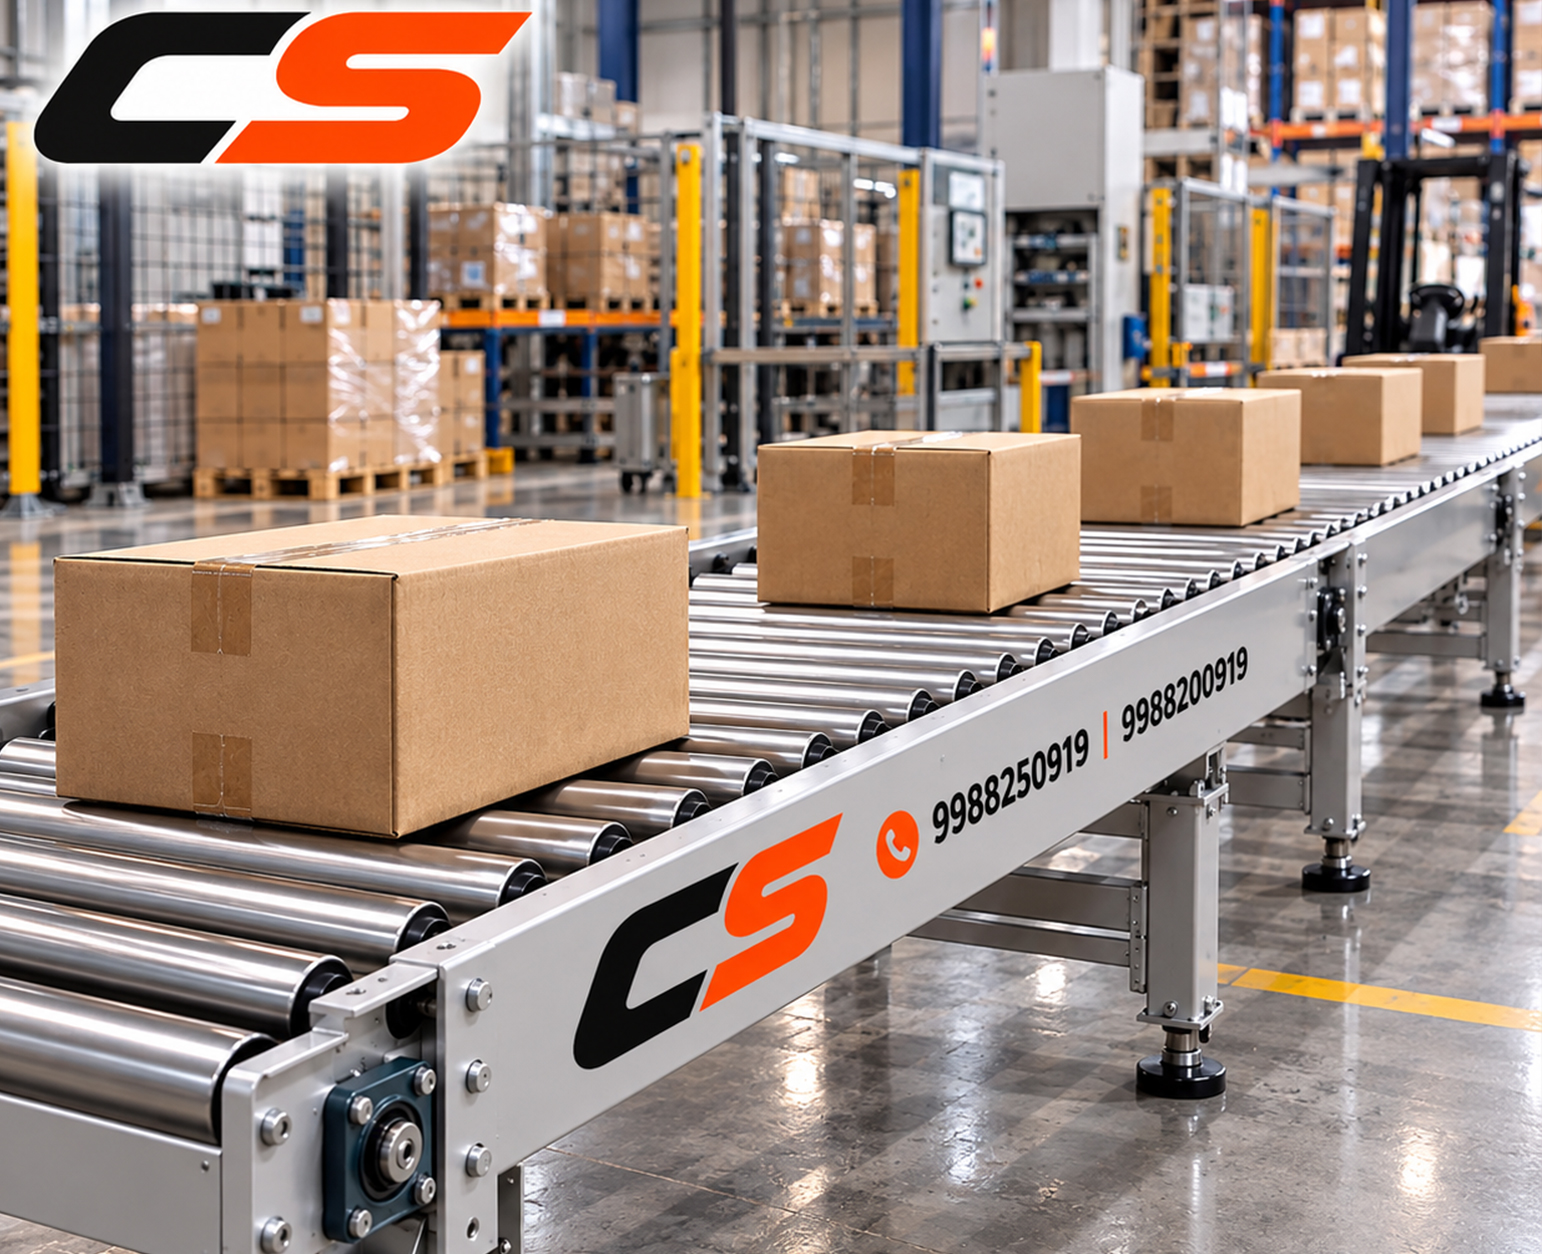
Our Images Gallery
Your Questions About Our
Conveyor Systems & Solutions
What types of conveyor systems do you provide?
We provide a wide range of conveyor systems including belt conveyors, modular conveyors, cleated conveyors, flat belt conveyors, inclined conveyors, bend conveyors, roller conveyors, and customized material handling systems.
Can you provide customized conveyor systems?
Yes. We design and manufacture customized conveyor systems according to your specific application, product dimensions, conveyor length, load capacity, layout, speed, and material handling requirements.
Which industries use your conveyor systems?
Our conveyor solutions are suitable for manufacturing, packaging, warehousing, logistics, food processing, automotive, pharmaceutical, recycling, and various other industrial applications.
What materials can be transported using your conveyors?
Our conveyors can handle a wide variety of products and materials, including cartons, boxes, bags, components, packaged goods, bulk materials, and other industrial products depending on the conveyor design.
Do you provide conveyor installation services?
Yes. We can provide complete installation and commissioning support to ensure that the conveyor system is properly installed, aligned, tested, and ready for reliable operation.
How do you ensure conveyor system quality?
We focus on quality materials, robust construction, precise fabrication, reliable components, and thorough inspection to ensure smooth operation, durability, and long-term performance.
Can conveyor systems be integrated with automation?
Yes. Our conveyor systems can be designed to work with industrial automation, sensors, control systems, sorting equipment, and other material handling solutions to improve production efficiency.
Why choose Conveyor Systems?
We focus on reliable products, customized engineering, quality workmanship, timely delivery, efficient material handling, and customer satisfaction. Our solutions are designed to provide dependable performance and long-term value.